
High-Performance Boiler Components & Flange Assemblies
Explore certified industrial pipe fittings, carbon steel elbows, forged flanges, and process control valves manufactured to international ISO/ASME/JIS engineering specifications.
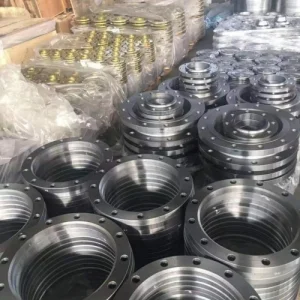
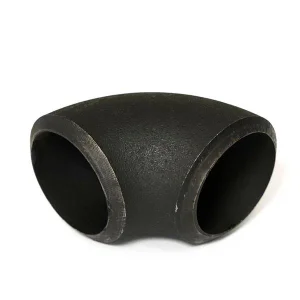
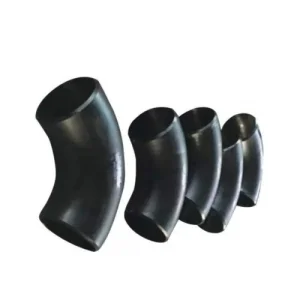
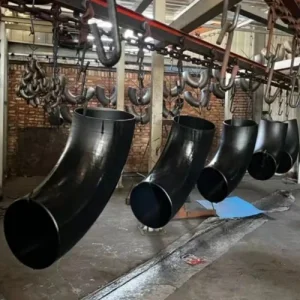
China Carbon steel elbows 90-Degree Elbow 45-Degree Elbow Manufacturers, Exporter
View Details & Pricelist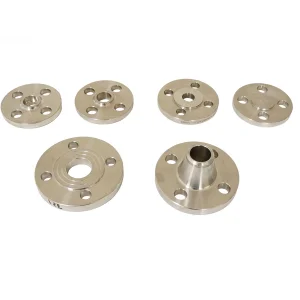
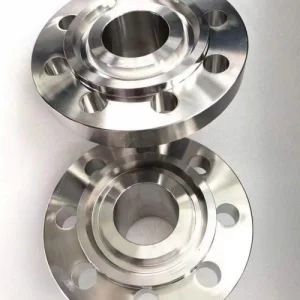
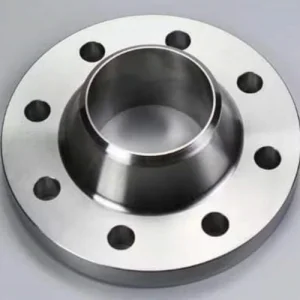
Wholesale B16.5 Duplex 2205 Stainless Steel Weld Neck Flange Blind Flange Manufacturers, Companies
View Details & Pricelist
Engineering Fundamentals of Boiler Condensate Pipe Systems
Analyzing water chemistry dynamics, carbonic acid formation, velocity thresholds, and alloy metallurgy for high-efficiency steam condensate return networks.
Carbonic Acid Corrosion Mechanisms
When high-pressure steam condenses back into liquid water within return lines, residual carbon dioxide ($\text{CO}_2$) gas dissolves into the unbuffered condensate. This reaction forms carbonic acid ($\text{H}_2\text{CO}_3$), dropping system pH levels down to 4.5 – 6.0.
Unprotected standard carbon steel pipes suffer rapid grooving along the bottom quadrant of horizontal lines. Selecting correct wall thicknesses (SCH 80/160) or alloy grades (ASTM A312 TP316L) prevents catastrophic thinning and plant downtime.
Two-Phase Flow & Erosion-Corrosion
Boiler condensate networks rarely handle pure liquid; they transport a turbulent two-phase mixture of flash steam and hot liquid water. As condensate drops in pressure across steam traps, flash steam expands rapidly, raising fluid velocities above 15 m/s.
Excessive velocity strips protective iron oxide passivating layers from elbow throats and tees. Engineering designs require wide-radius 1.5D or 3D seamless bend fittings to distribute fluid shear forces evenly.
Metallurgical Material Selection
Industrial boilers demand precise material pairing based on operating pressure and water treatment regimes:
- ASTM A234 WPB / A106 Gr.B: Economical choice for amine-treated low-pressure systems with heavy wall schedules.
- ASTM A403 WP304L / WP316L: Essential for acidic, unbuffered condensate lines requiring zero iron contamination.
- Duplex 2205 (UNS S31803): Applied in high-pressure power plant headers subject to chloride stress corrosion cracking.
Boiler Condensate Pipe Pricelist Benchmark & Cost Drivers
Direct factory-gate pricing reference table and cost structural analysis for international procurement teams and EPC estimators.
Procuring boiler condensate piping requires balancing initial capital expenditure against lifecycle maintenance costs. Carbon steel pipe options (A234 WPB) feature lower upfront unit costs but require routine chemical treatment (neutralizing amines) and thicker corrosion allowances (SCH 80/XS). Conversely, stainless steel (TP304L/TP316L) or duplex alloys eliminate corrosion allowances, drastically reducing line weight and long-term operating costs.
| Nominal Pipe Size (NPS) | Material Specification | Wall Schedule | Pressure Class | Estimated FOB Unit Price Range (USD) | Recommended Joint Interface |
|---|---|---|---|---|---|
| 1/2" (DN15) | ASTM A234 WPB Carbon Steel | SCH 80 / XS | Class 3000 / 150# | $2.80 – $4.50 / m | NPT Threaded / Socket Weld |
| 1" (DN25) | ASTM A403 WP304L Stainless | SCH 40S | Class 150# / PN16 | $8.50 – $12.20 / m | Butt-Weld / RF Flange |
| 2" (DN50) | ASTM A403 WP316L Stainless | SCH 40S | Class 300# / PN40 | $18.00 – $24.50 / m | Butt-Weld / WNRF Flange |
| 4" (DN100) | Duplex 2205 (UNS S31803) | SCH 80S | Class 600# / PN63 | $52.00 – $68.00 / m | Butt-Weld / RTJ Flange |
| 6" (DN150) | ASTM A106 Gr.B / A234 WPB | SCH 160 / XXS | Class 900# / PN100 | $45.00 – $58.00 / m | Butt-Weld Neck Flange |
| 8" (DN200) | ASTM A335 P11 Alloy Steel | SCH 80 | Class 600# / PN63 | $65.00 – $82.00 / m | High-Temp Butt Welding |
Key Pricelist Surcharge Drivers:
Prices vary based on global nickel/molybdenum alloy surcharges, non-destructive testing requirements (Radiographic 100% RT vs. Ultrasonic UT), heat treatment processes (Normalizing/Solution Annealing), and export packaging standards (wooden crates vs. steel bundles).
Macro Industrial Boiler Piping Infrastructure Integration
Tailored fluid transport architectures engineered for modern thermal power stations, petrochemical refineries, and combined heating networks.
Thermal Power Plants & HRSG Units
Heat Recovery Steam Generators (HRSG) operating in combined-cycle gas turbine (CCGT) plants demand rapid thermal cycling endurance. Our seamless carbon and alloy condensate return headers withstand high pressure-temperature fluctuation without thermal fatigue cracking.
Petrochemical & Refinery Process Lines
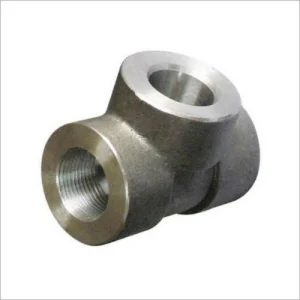
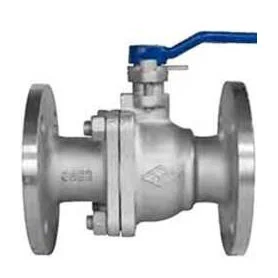
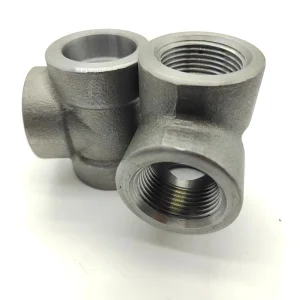
Refineries run extensive steam tracing networks to keep heavy crude fluids viscous. We supply full packages—including stainless steel ball valves (Q41F), forged tees, and slip-on flanges—guaranteeing zero leak rates in hazardous, corrosive atmospheric zones.
Municipal District Heating Infrastructure
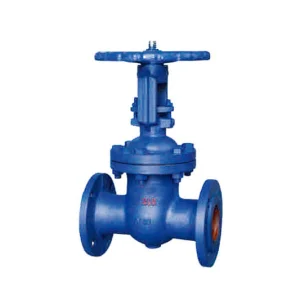
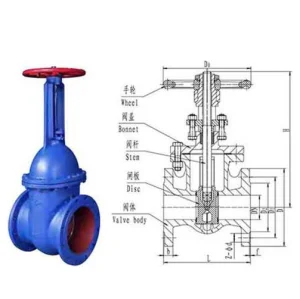
Large-scale urban steam networks rely on heavy-wall pre-insulated condensate pipes. Our factory supplies butt-weld carbon steel elbows and soft seal gate valves (Z45X) designed to handle multi-kilometer high-volume fluid return with minimal friction drop.
China Industry 4.0: Manufacturing Ecosystem & Supply Chain Resilience
How Cangzhou’s industrial pipe cluster empowers global buyers with automated forging precision, stringent testing, and integrated multi-factory supply chains.
Single-Source Procurement Advantage
Operating from Cangzhou, Hebei—China's primary industrial pipeline hub—HEBEI CANGRUN PIPELINE EQUIPMENT CO., LTD. along with its specialized production subsidiaries, CANGZHOU FEIWO METAL PRODUCTS CO., LTD. and CANGZHOU FEIXIANG METAL PRODUCTS CO., LTD., operates an end-to-end manufacturing footprint.
By consolidating raw steel billet sourcing, automatic hot-push elbow forming, CNC flange lathe machining, and valve assembly under a unified quality assurance system, we eliminate cross-vendor tolerances and shorten delivery lead times by up to 35%.
- Automated Forging & CNC Machining: Precision flange sealing faces (RF, FF, RTJ) machined to micron tolerances.
- Full Material Traceability: Complete Mill Test Reports (MTR) provided per EN 10204 3.1 / 3.2.
- Integrated Logistics Management: Active tracking of container bookings, port congestion buffer windows, and peak season surcharges (PSS).
Quality Assurance & Inspection Protocol
Future Outlook: Next-Generation Boiler Condensate Innovations
Preparing industrial piping systems for carbon-neutral steam generation, hydrogen co-firing, and AI-driven predictive corrosion monitoring.
IoT Smart Ultrasonic Corrosion Sensors
Future condensate return lines will embed non-invasive continuous ultrasonic thickness transducers into high-risk elbow bends. Connected to plant IoT control centers, these sensors predict wall-thinning rates in real time, shifting maintenance from reactive shutdowns to predictive servicing.
Nanostructured Anti-Scaling Internal Coatings
Advanced chemical vapor deposition (CVD) methods are applying hydrophobic nanostructured ceramic linings within pipe bores. These surface modifications lower condensate drop friction, eliminate scale build-up, and increase thermal energy retention by over 12% across long-distance distribution.
Zero Liquid Discharge (ZLD) Integration
As environmental regulations tighten global effluent discharge standards, modern boiler plants are transitioning to ZLD closed-loop condensate recovery. High-purity stainless steel (316L/Duplex 2205) piping components guarantee total fluid isolation, preventing chemical leaching into recycled feed water.
Global Enterprise Procurement Requirements & QA/QC Compliance
Meeting the stringent quality qualification frameworks mandated by global EPC contractors, engineering consultants, and international regulatory bodies.
ASME & Pressure Equipment Directive (PED)
Piping systems intended for power boilers must strictly adhere to ASME BPVC Section I & VIII alongside ASME B31.1 Power Piping Code. For European destinations, full compliance with the Pressure Equipment Directive (PED 2014/68/EU) CE marking ensures seamless field installation approval.
Dimensional & Threading Uniformity
Procurement teams require total alignment across international standards. We supply fittings certified to JIS B2311 / B2312 / B2313, GB/T 12459, and ANSI/ASME B16.9 / B16.11, featuring NPT, BSPT, or socket-weld joint ends engineered for rapid field assembly.
Export Packaging & Anti-Corrosion Protection
Ocean transit protection is critical. All carbon steel condensate components receive black anti-corrosion varnish, plastic end caps, and custom IPPC-certified ISPM-15 heat-treated wooden crate packing to survive high-humidity ocean voyages.
Frequently Asked Questions (FAQ) for Procurement & Engineering
Addressing core technical questions, pricing queries, material selection criteria, and export shipment specifications.
What is the main cause of failure in boiler condensate pipes?
The primary cause of failure is carbonic acid corrosion caused by dissolved CO2 gas in unbuffered condensate water, combined with erosion-corrosion from high-velocity flash steam expansion across steam traps. Using extra-heavy schedule carbon steel or stainless steel (304L/316L) mitigates this risk.
How do carbon steel (A234 WPB) and stainless steel (316L) compare in pricing?
Carbon steel fittings and pipes carry a significantly lower upfront purchase price (approximately 60-70% cheaper per meter than stainless). However, stainless steel 316L offers superior corrosion immunity, zero chemical dosage maintenance, and longer service life, making its total cost of ownership (TCO) lower in aggressive condensate environments.
Which standards do your company's fittings and flanges comply with?
Our products comply fully with international standards including ASME/ANSI B16.9, B16.11, B16.5, JIS B2311/B2312/B2313, EN 10253, and GB/T 12459. Pressure ratings span Class 150 to Class 2500, and PN2.5 to PN400.
What size ranges are available for seamless fittings and forged flanges?
We manufacture seamless butt-weld fittings from 1/2" up to 24" (DN15–DN600), welded fittings up to 78" (DN1900) with wall thicknesses up to 150mm, and forged weld neck flanges up to 160" (DN4000).
Can you provide customized MTR and third-party inspection certificates?
Yes. Every batch is supplied with EN 10204 3.1 Mill Test Reports detailing chemical composition and mechanical properties. Third-party inspection (TPI) by SGS, BV, TUV, or Lloyd's Register is available upon request.
What is the typical export lead time for global project orders?
Standard stock fittings and forged flanges ship within 7 to 10 days. Customized alloy or large-diameter seamless pipe packages typically require 20 to 30 days for production, NDT testing, and export packing.
Forged Fittings, Heavy Industrial Valves & Specialized Flanges
Complete your boiler piping bill of materials with our high-pressure forged NPT fittings, gate valves, cast stainless components, and WNRF flanges.
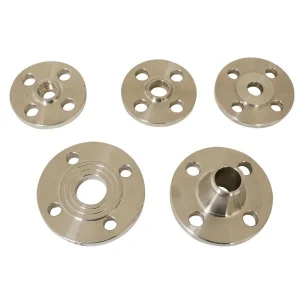
China DIN Class150 Stainless Steel Butt Weld So Slip on Flange Manufacturers, Supplier
View Details & Pricelist
Request an Instant Project Quote & Technical Catalog
Send your bill of materials (MTO) directly to our engineering team. Receive comprehensive factory-direct pricelists, CAD dimensional drawings, and material certification packages within 24 hours.
Contact Our Global Export Department