
Industrial Pipe Caps & Fittings Showcase
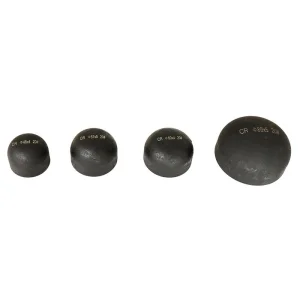
Explore precision-engineered ASME B16.9 butt-weld caps, threaded end caps, and high-integrity pressure vessel enclosures manufactured by Cangrun Pipeline.
Global Macro-Industry Landscape for Industrial Pipe Caps
Analyzing global demand shifts across energy, petrochemical, cryogenic, and municipal piping networks.
The Critical Role of Pipe Caps in System Integrity
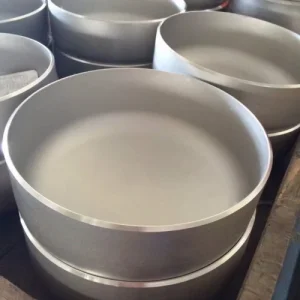
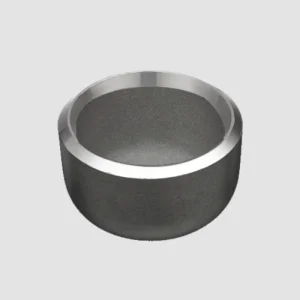
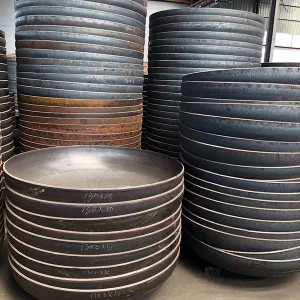
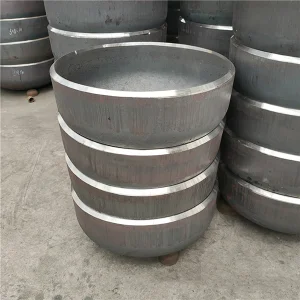
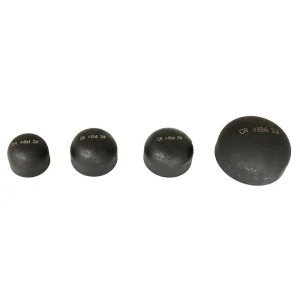
In modern industrial process plants, pipe end caps—often referred to as dished heads or blind ends—serve a fundamental safety and structural purpose. Unlike temporary closures, permanent butt-weld caps manufactured according to ASME B16.9 or EN 10253 are designed to withstand full line pressure, thermal cycling, and aggressive chemical environments. They terminate dead-ends, line extensions, manifold headers, and pressure vessel nozzles with absolute mechanical reliability.
As global infrastructure transitions toward clean energy—including hydrogen blending networks, ultra-deepwater oil extraction, and high-efficiency LNG re-gasification plants—the technical demand placed on cap manufacturers has increased dramatically. Modern caps are no longer simple stamped metal plates; they are precision-formed pressure components subjected to stringent finite element analysis (FEA) and destructive testing.
Global Procurement Trends & Demand Dynamics
Major EPC (Engineering, Procurement, and Construction) firms are systematically shifting their sourcing strategies toward integrated manufacturing clusters. Cangzhou, Hebei has established itself as the global epicenter for industrial pipe fitting production. By consolidating material purchasing, hot forging, heat treatment, and non-destructive testing (NDT) within a single region, cap companies can offer unparalleled cost efficiency without compromising technical compliance.
Key growth drivers in the global market include:
- LNG & Cryogenic Projects: High demand for low-temperature nickel-alloy and austenitic stainless caps (ASTM A403 WP316L / A420 WPL6) operating at -196°C.
- Subsea Pipeline Infrastructure: Deepwater applications requiring high-yield carbon steel caps (ASTM A860 WPHY60/70) with heavy wall thicknesses up to 150mm.
- Refinery Hydrocarbon Units: High-temperature alloy caps (ASTM A234 WP91/WP22) capable of enduring severe creep and hydrogen attack.
Engineering Standards & Geometric Design Framework
Deep technical specifications comparing ASME B16.9, DIN 2617, and EN 10253 pressure vessel geometries.
Mathematical Ellipsoidal Head Geometry (2:1 Ratio)
The standard ASME B16.9 factory-made wrought butt-welding cap features a 2:1 semi-ellipsoidal geometry. This specific profile ensures that membrane stresses across the dome are evenly distributed, minimizing localized stress concentrations at the knuckle radius where the curved head transitions into the straight cylindrical skirt.
The structural thickness requirement of a seamless ellipsoidal cap under internal pressure is governed by the ASME Boiler & Pressure Vessel Code (BPVC) Section VIII, Division 1, calculated as follows:
Where: t = Minimum required wall thickness; P = Internal design pressure; D = Inside diameter of cap skirt; S = Maximum allowable stress value of material; E = Joint efficiency factor (typically 1.00 for seamless wrought fittings).
| Standard Code | Material Classification | Size Range (NPS / DN) | Schedule / Pressure Rating | Key Geometric Features |
|---|---|---|---|---|
| ASME / ANSI B16.9 | Carbon, Alloy, Stainless Steel | 1/2" to 78" (DN15 - DN1900) | SCH 10S to SCH XXS, max 150mm | 2:1 Ellipsoidal head with straight cylindrical skirt for butt welding |
| MSS SP-43 | Austenitic Stainless & Duplex | 1/2" to 24" (DN15 - DN600) | Lightweight SCH 5S and SCH 10S | Designed for low-pressure corrosion-resistant process piping |
| EN 10253-2 / -4 | Non-alloy, Alloy & Austenitic | DN15 to DN1200 | Type A (Equal wall) / Type B (Full pressure) | Torispherical shape according to DIN 28011 (Kloepper head) |
| JIS B2311 / B2312 | SGP, STPT, SUS Grades | 15A to 1500A | 10K, 20K, Sch 40 to Sch 80 | Japanese industrial standard for general and pressure pipeline services |
| DIN 2617 | St37.0, St35.8, 15Mo3 | DN15 to DN1000 | PN10 to PN100 | German standard welded pipe end caps with standardized rim height |
Metallurgical Science & Material Selection Matrix
Analyzing grain structure, chemical compositions, and thermal treatments for extreme operational environments.
Carbon & Low-Temp Alloy Steels
ASTM A234 WPB & WPC: The standard wrought carbon steel grade for medium to high-temperature service. Fully killed steel with controlled Carbon (max 0.30%), Manganese (0.29-1.06%), and Silicon (min 0.10%) ensures superior weldability and ductility.
ASTM A420 WPL6: Formulated for sub-zero operations down to -45°C. Requires fine-grain aluminum-killed melt practice and normalizing heat treatment to guarantee minimum Charpy V-Notch impact values of 18 ft-lbs (25 J) at design temperatures.
Austenitic & Duplex Stainless Steels
ASTM A403 WP304/304L & WP316/316L: 304L provides excellent resistance to atmospheric corrosion and oxidizing media. 316L, containing 2.0-3.0% Molybdenum, is critical for resisting localized pitting and crevice corrosion in chloride-rich environments.
Duplex 2205 (UNS S31803 / S32205) & Super Duplex 2507: Ferritic-austenitic dual-phase microstructure providing twice the yield strength of conventional austenitic stainless steel alongside exceptional stress corrosion cracking (SCC) resistance.
High-Temperature Chromium-Moly Alloys
ASTM A234 WP11, WP22, WP91, WP911: Alloyed with Chromium (up to 9.0%) and Molybdenum (up to 1.0%) to prevent graphitizing and maintain mechanical creep strength at thermal continuous limits exceeding 600°C.
WP91 (9Cr-1Mo-V) caps require stringent double-heat treatment—normalizing at 1040°C followed by tempering at 760°C—to develop a fully tempered martensitic microstructure capable of withstanding extreme boiler pressures.
Manufacturing Precision & Quality Assurance Roadmap
From raw plate deep-drawing to automated beveling and advanced non-destructive inspection.
Advanced Hot Pressing & Cold Forming Methods
Cangrun Pipeline utilizes multi-stage hydraulic deep-drawing presses ranging from 500 to 5,000 metric tons capacity. The manufacturing route is selected based on wall thickness and metallurgical requirements:
- Cold Deep Drawing: Applied to stainless steel and thin-wall carbon caps (up to SCH 40S). Plate circular blanks are lubricated and drawn through precision dies, followed by immediate solution annealing to restore grain structure.
- Hot Deep Drawing / Forging: Mandatory for heavy-wall alloy and carbon steel caps. Steel plates are induction heated to 1050°C - 1150°C before hydraulic forming, ensuring zero internal micro-tearing.
- Machining & Beveling: Skirts are CNC-machined to conform to ASME B16.25 weld bevel profiles (37.5° ± 2.5° with 1.6mm root land), guaranteeing seamless field alignment with adjacent seamless pipe.
Non-Destructive Testing (NDT) & Quality Verification
Every cap manufactured across Cangrun's facilities undergoes rigorous quality inspection prior to tagging and dispatch:
- Ultrasonic Testing (UT): 100% volumetric examination of raw steel plates and finished caps per ASME Section V to detect laminations, inclusions, or sub-surface voids.
- Radiographic Testing (RT): Applied to welded-construction large-diameter caps (DN600+) to verify full-penetration weld seam integrity.
- Positive Material Identification (PMI): X-ray fluorescence (XRF) testing on every stainless, duplex, and alloy cap to verify chemical compliance against MTR specs.
- Hydrostatic Testing & Hardness Testing: Hardness checks (Rockwell/Brinell) confirm compliance with NACE MR0175 / ISO 15156 sour service requirements (max 22 HRC).
Industry-Specific Macro Solutions
Tailored cap engineering across major global industrial market segments.
Offshore Oil & Gas Pipelines
High-yield caps (ASTM A860 WPHY52, WPHY65) designed to endure wave loading, ocean floor movement, and high internal pressure up to Class 2500. Features 100% UT lamination checks and heavy-duty anti-corrosion FBE (Fusion Bonded Epoxy) exterior coatings.
Refinery & Petrochemical Crackers
Chrome-Moly (WP91/WP22) caps optimized for high-temperature catalytic cracking and hydroprocessing units. Resist hydrogen attack, thermal shock, and thermal expansion fatigue up to 650°C continuous operation.
Cryogenic LNG Storage Terminals
Austenitic stainless (316L) and 9% Nickel alloy caps engineered for liquid natural gas transport at -196°C. Guaranteed impact toughness down to ultra-cryogenic regimes prevents brittle catastrophic fracture.
Enterprise Procurement Strategy & Global Compliance
Mitigating supply chain risks, total cost of ownership (TCO), and international regulatory requirements.
Total Cost of Ownership (TCO) & Sourcing Optimization
Procuring pipe caps for major industrial infrastructure projects involves far more than comparing initial unit pricing. Overseas procurement directors must evaluate the complete TCO equation, incorporating freight surcharges, non-conformance risks, material test report (MTR) verification, and project downtime costs.
Cangrun Pipeline optimizes enterprise procurement through:
- Material Consolidation: Purchasing caps, elbows, tees, flanges, and seamless pipes under a single consolidated purchase order, maximizing container payload and reducing sea freight costs per ton.
- Traceability & EN 10204 3.1/3.2 Certification: Full heat-number traceability mapped directly from raw steel mill heat receipts to final hydro-tested caps. Third-party inspection (SGS, BV, TUV, DNV) supported.
- Export Logistics Buffer Management: Real-time tracking of global ocean freight trends, port congestion warnings, and carrier surcharges to protect project delivery windows.
International Certification & Regulatory Harmonization
Cap manufacturers must maintain a robust suite of global quality approvals to satisfy local plant operating regulations:
- PED 2014/68/EU (Pressure Equipment Directive): Mandatory compliance for pipe fittings installed across the European Economic Area (EEA), featuring CE marking and Module H full quality assurance certification.
- ASME BPV Code Certification: Authorized manufacture under ASME Section VIII rules for pressure vessel closure caps.
- Canadian Registration Number (CRN): Technical design registration across all Canadian provinces and territories for pressurized fitting lines.
- ISO 9001:2015 / ISO 14001 / ISO 45001: Fully integrated quality, environmental, and occupational health management systems.
Technical Roadmap & Future Outlook (2025–2030)
Smart manufacturing, AI-assisted quality control, and sustainable green steel fitting production.
AI-Assisted Ultrasonic Defect Detection
Integration of real-time machine learning algorithms into automated ultrasonic testing rigs. Automated defect recognition (ADR) analyzes ultrasonic echo signals at microsecond speeds, eliminating human interpretation variance during volumetric plate scanning.
Green Steel & Low-Carbon Forging
Transitioning manufacturing operations toward hydrogen-fueled reheat furnaces and scrap-based Electric Arc Furnace (EAF) steel sourcing. Reduces the embedded carbon footprint of Cangrun fitting products by up to 45% by 2028.
Smart Digital Twins & QR Heat Tracking
Laser-engraved 2D DataMatrix codes on every cap skirt. Plant operators can scan the physical fitting on-site to instantly display MTR certificates, FEA stress reports, wall thickness maps, and installation torque guidelines.
Frequently Asked Questions (Procurement & Technical FAQ)
Expert engineering answers to common inquiries raised by buyers, piping designers, and quality inspectors.
Comprehensive Pipe Fittings, Flanges & Valves Portfolio
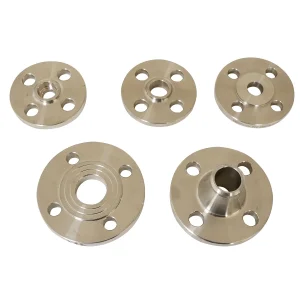
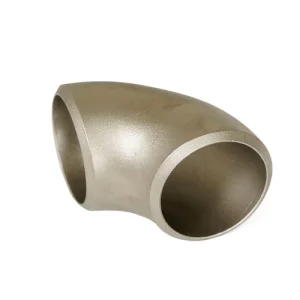
Explore additional high-grade pipe closure caps, forged flanges, and process components engineered by Cangrun Pipeline group factories.
HEBEI CANGRUN PIPELINE EQUIPMENT CO., LTD.
Headquartered in Bobei Industrial Zone, Cangzhou, Hebei, China, Cangrun Pipeline operates as a world-class manufacturing group together with its dedicated production subsidiaries, CANGZHOU FEIWO METAL PRODUCTS CO., LTD. and CANGZHOU FEIXIANG METAL PRODUCTS CO., LTD. (Boerzhuang Industrial Zone).
Specializing in ASME/ANSI, EN/DIN, JIS, and GB standard butt-weld caps, elbows, tees, reducers, forged flanges, seamless steel pipes, and industrial valves for major global EPC contractors and distributors.