
Featured Piping Components for Hungarian Infrastructure
Certified high-yield steel flanges, heavy-wall pipe tees, and long-radius elbows fully compliant with EN 10253, EN 1092-1, and ASME B16.9 specs for Central European project contractors.
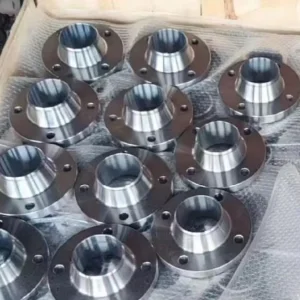
Wholesale Stainless Steel 304 Weld Neck Flange & Custom Carbon Steel Flanges for Hungary Projects
View Product Specifications →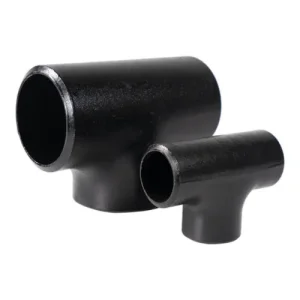
China Heavy-Duty Equal & Reducing Pipe Tee Factory Direct Supply for Hungarian Engineering
View Product Specifications →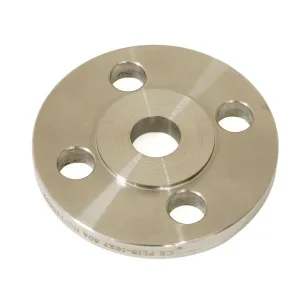
Famous Stainless Steel & Carbon Steel Water Pipe Standard Blind Flange Supplier for Hungary
View Product Specifications →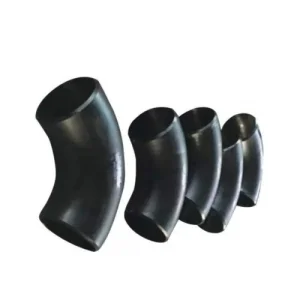
High-Quality Long & Short Radius Pipe Elbow Factories & Exporters Serving Central Europe
View Product Specifications →Hungary’s Industrial Transformation & Strategic Piping Requirements
Analyzing Central Europe's evolving energy, chemical, and manufacturing corridor and the stringent technical benchmarks required for cross-border pipeline procurement.
1. Geothermal Energy & District Heating Networks
Hungary sits atop one of Europe’s richest thermal water reservoirs. Cities such as Szeged, Miskolc, and Budapest are aggressively expanding geothermal district heating loops to replace fossil fuels. These geothermal networks require high-frequency induction bends and corrosion-resistant alloy piping systems capable of handling mineralized brine, thermal shocks, and continuous cyclic pressure up to PN25/PN40.
Our induction bends feature smooth directional transitions (3D, 5D, 8D bend radii) that minimize flow turbulence and head loss, dramatically lowering pump energy consumption across municipal heating grids.
2. Petrochemical Refining & Gas Interconnectors
The MOL Százhalombatta Refinery (Danube Refinery) and Hungary’s expanding natural gas cross-border interconnectors (BRUA pipeline corridor, Serbo-Hungarian interconnector) demand high-yield steel pipe bends (API 5L X52, X65, X70) and heavy-wall carbon/alloy steel fittings (ASTM A234 WPB, WP11, WP22, WP91).
Pipeline bends destined for high-pressure gas transport must strictly comply with EU Pressure Equipment Directive (PED 2014/68/EU) and EN 10253 standards, ensuring 100% volumetric Non-Destructive Testing (NDT) to prevent structural failure under extreme operational stresses.
Technical Deep-Dive: High-Frequency Induction Bends vs. Standard Elbows
Why EPC contractors in Hungary prefer custom-engineered induction bends over conventional short-radius elbows for critical oil, gas, and power applications.
Optimal Hydrodynamics & Piggability
Induction bends provide custom bend angles from 1° to 180° with long radiuses (R = 3D, 5D, 6D, 8D, 10D). Unlike 1.5D standard elbows, long-radius induction bends permit smooth passage of pipeline inspection tools (smart pigs) and scrapers, which is vital for Hungary's long-distance transit gas lines and oil transmission pipelines.
Wall Thinning & Ovality Control
During induction bending, medium-frequency electrical induction coils heat a narrow circular band of the pipe while pushing it around a pivoting arm. Our computer-controlled bending speed and hydraulic push forces strictly limit extrados wall thinning to <10% and maintain ovality ratio below 3%, adhering to stringent EN 12952 and ASME B31.3 codes.
Post-Bend Heat Treatment (PWHT)
Bending high-yield carbon steels (X70/WPB) or chrome-moly alloy steels (A335 P91/P22) alters microstructural grain boundaries. Cangrun Pipeline subjects all finished bends to full-body normalizing, quenching, and tempering (N+T / Q+T) in computerized heat-treatment furnaces to restore yield strength, tensile toughness, and Charpy V-notch impact values at -40°C.
| Performance Parameter | High-Frequency Induction Bend | Standard Butt-Weld Elbow (1.5D) | Cold Miter Bend |
|---|---|---|---|
| Available Bend Radii | 3D, 5D, 6D, 8D, 10D to 20D (Custom) | 1.0D (Short) & 1.5D (Long) | Segmented Angle Joints |
| Pressure Loss & Friction | Extremely Low (<5% pressure drop) | Moderate Friction Losses | High Turbulence & Erosion Risk |
| Pig Passability (Piggable) | 100% Compatible with Smart Pigs | Restricted / Requires Special Pigs | Not Piggable |
| Weld Seam Density | Zero circumferential welds in bend body | Requires multiple circumferential welds | Multiple high-stress welded segments |
| Structural Integrity | Continuous material, full PWHT grain recovery | Standard forged/formed structural strength | High stress concentration at miter joints |
China Manufacturing Ecosystem & Hebei Cangrun Advantage
Combining Cangzhou’s world-renowned pipeline manufacturing industrial cluster with seamless logistics to deliver unmatched cost efficiency and technical quality to Hungary.
Integrated Group Manufacturing Power
Hebei Cangrun Pipeline Equipment Co., Ltd., operating alongside its specialized production facilities—Cangzhou Feiwo Metal Products Co., Ltd. and Cangzhou Feixiang Metal Products Co., Ltd.—forms a complete pipeline manufacturing ecosystem in Hebei Province.
By controlling raw steel billet sourcing from tier-1 steel mills (Baosteel, TPCO, Shougang), hot forging, induction bending, precision CNC machining, and automated anti-corrosion coating under one group, we offer Hungarian procurement teams a unified procurement package: matching pipe, fittings, flanges, and valves in exact material heat numbers.
Optimized Logistics Corridor to Central Europe
Delivery speed and freight predictability are paramount for European engineering contractors. Our dedicated export logistics desk manages multi-modal freight routes specifically tailored for Central European destinations:
- China-Europe Railway Express (Yiwu/Zhengzhou to Budapest BILK Terminal): 16-18 days transit time, bypassing maritime choke points for urgently required project fittings.
- Direct Maritime Shipping via Koper / Rijeka Ports: Cost-effective ocean containerized or breakbulk shipping serving landlocked Hungary via Adriatic rail connections.
Localized Application Scenarios in Hungary's Key Industrial Hubs
Tailored metallurgical and structural solutions designed for major regional projects across Hungary.
Debrecen EV Battery Megafactories
With major investments in electric vehicle battery production (e.g., CATL, Eve Energy in Debrecen), high-purity water handling, solvent piping, and chemical utility lines require ASTM A403 WP304L/316L stainless steel seamless pipe bends, tees, and sanitary flanged ball valves featuring ultra-low carbon chemistry to prevent intergranular corrosion.
Paks II Nuclear Power Expansion
Nuclear secondary cooling loops and steam piping demand high-temperature alloy steel bends (ASTM A335 P11, P22, P91) certified with EN 10204 3.2 inspection certificates (witnessed by TÜV SÜD or DNV). Every bend undergoes 100% Ultrasonic Testing (UT) and Radiographic Testing (RT).
Győr & Kecskemét Automotive Corridors
Heavy industrial automotive manufacturing plants rely on compressed air distribution lines, high-pressure hydraulic circuits, and boiler room utility lines using ASME B16.5 Class 150/300 forged A105 carbon steel weld neck flanges and PN16 soft-seal gate valves.
Quality Assurance & Risk Mitigation for European Procurement
How Hebei Cangrun Pipeline eliminates procurement risk for EU buyers through rigorous testing protocols and standard compliance.
EN 10204 3.1 & 3.2 Material Traceability
Every consignment delivered to Hungary includes comprehensive Material Test Reports (MTR) according to EN 10204 3.1. Chemical composition (carbon equivalent CE calculated), mechanical yield/tensile testing, hardness values (HBW/HV), and impact test data at freezing temperatures are fully documented and heat-number stamped onto each bend, flange, and fitting.
Third-Party Inspection Witnessing
We routinely collaborate with independent international inspection bodies—including SGS, TÜV, Bureau Veritas (BV), and Intertek—to perform pre-shipment inspections, dimensional verification, wall thickness ultrasonic gauge testing, hydrostatic testing, and surface coating dry-film thickness (DFT) checks.
Complete Industrial Piping Portfolio for Hungary Engineering Imports
Factory-direct forged flanges, high-pressure elbows, end caps, and industrial valves ready for export packaging and project delivery.
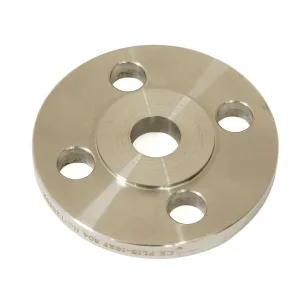
Famous ASME B16.5 Forged 2 Inch Blind ANSI Class 150 Carbon Steel Customized Flange Quotes for Hungary
View Product Specifications →
Famous Butt Weld Pipe Fittings End Cap A234WPB Carbon Steel Pipe Fitting Supplier Serving Hungary
View Product Specifications →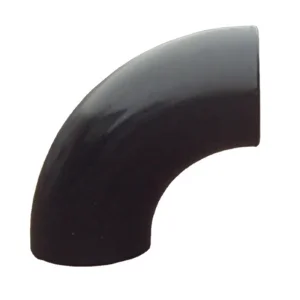
China Long/Short Radius 316 90 Degree Stainless Steel High Pressure Smooth Polishing Elbow for Hungary
View Product Specifications →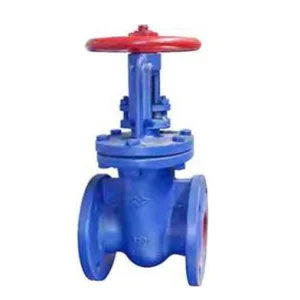
Buy Wedge Gate Valve A+Z41T/W-10/16 Direct Factory Pricelist & Product Quotes for Hungary Projects
View Product Specifications →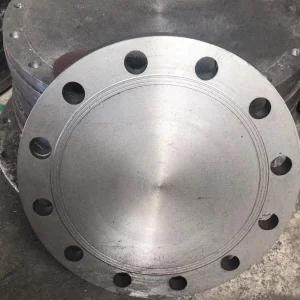
Famous ASME B16.9 / ANSI B16.47 Blind Flange & Heavy Forged Flange Manufacturer for Central Europe
View Product Specifications →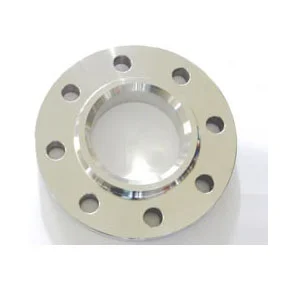
High-Quality Industrial Carbon Steel Slip On Weld Flange Exporter & Supplier to Hungarian Plants
View Product Specifications →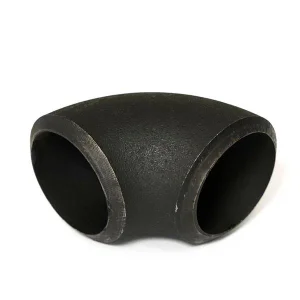
China Carbon Steel 90-Degree & 45-Degree Butt-Weld Elbow Manufacturers Exporter to Hungary
View Product Specifications →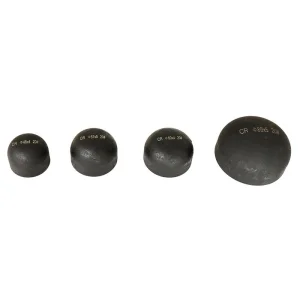
Best ASME Standard B16.9 Butt-Weld Steel Pipe Fittings Caps Factory Direct Quotes for Hungary Market
View Product Specifications →Frequently Asked Questions (FAQ) for Hungarian Pipe & Fitting Buyers
Clear answers regarding international standards, European PED certifications, shipping timelines, and custom engineering capabilities.
How do Cangrun induction bends comply with European standard EN 10253 and PED 2014/68/EU?
All pipe bends and pressure-containing fittings manufactured for the European Union market undergo stringent conformity assessment procedures under PED 2014/68/EU. Our manufacturing system is certified for EN 10253-2 (carbon steel) and EN 10253-4 (stainless steel), providing complete wall-thickness tolerance compliance and full EN 10204 3.1 material traceability.
What bend radii and outer diameter sizes can your Cangzhou factory produce?
Our induction bending machines handle pipe sizes from 1/2" up to 60" (DN15 to DN1500) with wall thicknesses up to 150 mm. We produce custom bend radii including 3D, 5D, 6D, 8D, and 10D at custom angles ranging from 1° to 180° with exact tangent leg lengths as required by project drawings.
What is the typical shipping lead time from China to Hungary for urgent pipeline projects?
For urgent requests, we utilize the China-Europe Railway Express (direct to Budapest BILK rail terminal), which takes approximately 16 to 18 days. Ocean freight shipments dispatched to the Port of Koper (Slovenia) or Port of Rijeka (Croatia) with inland rail feeder connection take approximately 28 to 35 days.
Can you supply complete matched packages of pipes, fittings, flanges, and valves together?
Yes. Because Hebei Cangrun operates as a consolidated group with specialized subsidiary plants (Cangzhou Feiwo Metal Products Co., Ltd. and Cangzhou Feixiang Metal Products Co., Ltd.), buyers can combine seamless steel pipes, induction bends, butt-weld tees, forged flanges, and ball/gate valves in a single container shipment with harmonized material test reports.
Request Factory-Direct Quotations for Hungary Projects
Send your material take-off (MTO) list or technical piping drawings to our engineering team. Receive detailed technical proposals, unit pricing, and EN 10204 compliance guarantees within 24 hours.