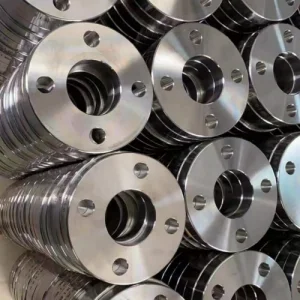
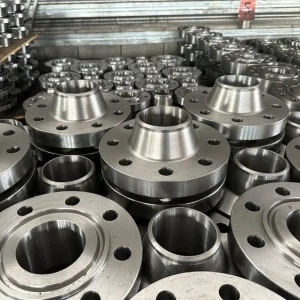
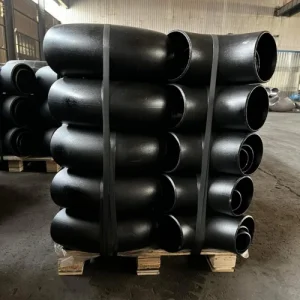
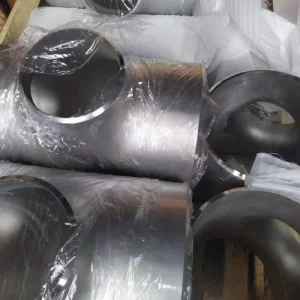
Featured Industrial Fittings & Flanges (Batch 01)
The Global Commercial & Engineering Status of DN1200 Gate Valves
Exploring the critical role of 48-inch (DN1200) heavy-duty Isolation valves across municipal mega-projects, thermal power circuits, seawater desalination, and transcontinental pipelines.
In modern industrial process engineering, the DN1200 (NPS 48) Gate Valve represents a pinnacle of mega-bore isolation technology. Designed to manage colossal volumetric flow rates under stringent hydraulic pressure regimes, DN1200 gate valves serve as indispensable fluid isolation control points in heavy civil works, municipal raw water transmission, agricultural irrigation schemes, thermal power plant cooling circuits, and downstream petrochemical facilities.
Globally, the market for large-bore gate valves has entered a phase of heightened capital expenditure. According to recent infrastructure intelligence reports, the global market valuation for large-diameter industrial valves (NPS 36 to NPS 72) is projected to exceed $14.8 Billion by 2030, driven heavily by urbanization in Asia-Pacific, aggressive water security infrastructure in the Middle East, and cross-border energy expansion initiatives in North America and Western Europe.
Wholesale Valuation & Capital Intensity
DN1200 valves require massive casting tonnages (often exceeding 6.5 to 12 metric tons per unit depending on pressure rating). Price quotes fluctuate based on raw metallurgical indices (WCB, Ductile Iron GGG50, Stainless CF8M) and actuator specifications.
Regional Procurement Shifts
Engineering, Procurement, and Construction (EPC) contractors are increasingly consolidating supply chains toward integrated Chinese manufacturers like Hebei Cangrun Pipeline Equipment Co., Ltd. to achieve optimal cost-per-performance metrics without compromising ASME B16.34 or EN 1171 compliance.
Quality & Life Cycle Standards
In large-bore water and industrial service, unplanned downtime carries immense financial risk. Today's procurement frameworks mandate double-block-and-bleed (DBB) capabilities, zero-leakage resilient wedge seating, and long-term anti-corrosive epoxy linings.
DN1200 Gate Valve Technical Roadmap & Design Paradigms
An engineering breakdown of mechanical configurations, pressure-temperature ratings, actuator gearboxes, and structural Finite Element Analysis (FEA).
Designing a gate valve with a nominal diameter of 1200mm requires overcoming massive hydraulic thrusts and stem torque constraints. When operating under working pressures of PN10, PN16, PN25, or Class 150/300, the differential force exerted against the gate disk when closed can easily exceed hundreds of kilonewtons. Engineering teams must evaluate key structural choices:
| Engineering Parameter | Resilient Seated (Z45X / AWWA C515) | Metal Seated (Z41H / API 600 / BS 5163) | Parallel Slide / Conduit Gate |
|---|---|---|---|
| Nominal Size | DN1200 / 48 Inches | DN1200 / 48 Inches | DN1200 / 48 Inches |
| Pressure Classes | PN6, PN10, PN16, Class 150 | PN10, PN16, PN25, PN40, Class 150-600 | PN16 to PN100, Class 150 to Class 900 |
| Body Metallurgy | Ductile Iron (EN-GJS-500-7 / A536 65-45-12) | Cast Steel (ASTM A216 WCB / LCC, A351 CF8M) | Forged Steel / Heavy WCB / Duplex 2205 |
| Seating Material | EPDM / NBR Encapsulated Ductile Wedge | Stellite Hardfaced / Stainless 13Cr Overlay | Metal-to-Metal Spring Loaded Seats |
| Operation Mode | Bevel Gearbox + Electric/Pneumatic Actuator | Multi-turn Electric Actuator (ROTORK/AUMA) | Hydraulic / High-Torque Electric Actuator |
| Typical Media | Potable Water, Neutral Liquid, Sewage | High Temp Steam, Crude Oil, Slurry, Gas | High Pressure Natural Gas, Refined Products |
Hydraulic Thrust Mitigation
To facilitate smooth opening without galling the seats or bending the stem, DN1200 gate valves are frequently customized with an integrated External Bypass Valve System (DN80 - DN150). Opening the bypass equalizes upstream and downstream pressure prior to main gate displacement.
Anti-Corrosion Fusion Coatings
Body and bonnet surfaces undergo shot-blasting to SA 2.5 cleanliness followed by electrostatic application of non-toxic Fusion Bonded Epoxy (FBE) coating at 250–350 microns thickness, complying with WRAS and AWWA C550 standards.
Stem & Drive Train Rigidity
Utilizing rolled or forged high-tensile Stainless Steel stems (AISI 420 / 316 / 17-4PH) with trapezoidal threads (ACME), combined with ISO 5210 top flanges for direct mounting of multi-turn smart actuators.
Integrated Piping Infrastructure: Valves, Flanges & Fittings
A large-bore DN1200 gate valve does not work in isolation. It relies on a balanced ecosystem of matching ASTM/ASME/EN flanges, heavy-wall butt-weld fittings, and steel pipes.
At Hebei Cangrun Pipeline Equipment Co., Ltd. (and our Cangzhou group manufacturing subsidiaries), we recognize that pipeline failure often occurs at transition points—where valves meet companion flanges or reducers. Procuring a complete piping package from a single qualified manufacturing group eliminates dimensional mismatches, wall thickness mismatches (Schedule 40/80/STD vs. custom PN ratings), and material grade inconsistencies.
Matching Piping Components for DN1200 Gate Valve Installations:
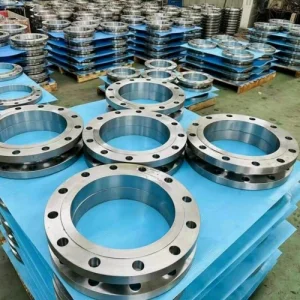
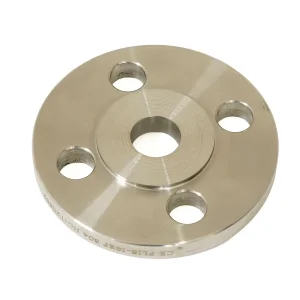
- Companion Weld Neck Flanges: ASME B16.47 Series A / Series B (DN1200 / 48 inch) or EN 1092-1 Type 11 PN10/PN16/PN25 flanges manufactured in ASTM A105, A350 LF2, or stainless A182 F304L/F316L.
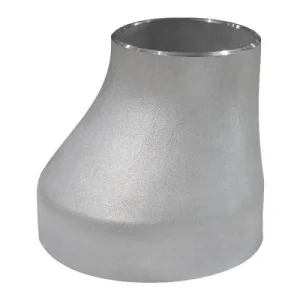
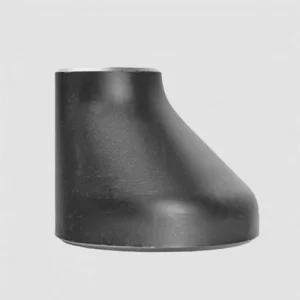
- Heavy-Wall Steel Reducers: Concentric and Eccentric Reducers (e.g., 60" to 48" or 48" to 40") in ASTM A234 WPB or WPC to step down line sizes while managing velocity head.
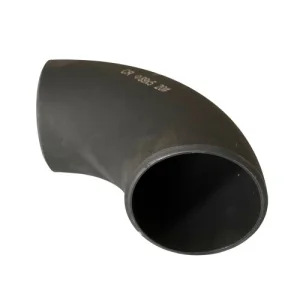
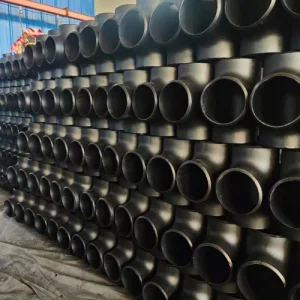
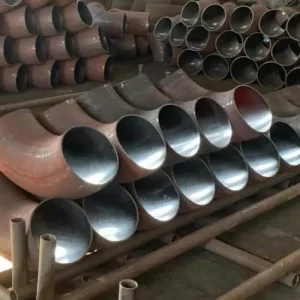
- High-Pressure Butt-Weld Fittings & Bends: Long Radius 1.5D / 3D / 5D steel pipe bends engineered for piggable lines adjacent to main gate valve stations.
- Sealing Systems: Spiral wound gaskets with inner/outer rings (SS316 + PTFE/Graphite) or Ring Type Joint (RTJ) metal gaskets for high-pressure oil/gas isolations.
Localized Application Scenarios & Macro Industry Solutions
How DN1200 Gate Valves and integrated piping systems solve critical fluid control challenges in key sectors worldwide.
Urban Water Supply & Flood Mitigation
Installed in municipal intake stations and storm surge barrier networks. Resilient seat DN1200 valves provide 100% drip-tight shutoff against raw river water and debris without wedge jamming.
Seawater Desalination Plants (SWRO)
High-salinity marine environments demand Super Duplex Steel (2205 / 2507) or rubber-lined Ductile Iron gate valves coupled with matching stainless flanges to withstand pitting and crevice corrosion.
Thermal & Nuclear Power Plants
Serving as main cooling tower isolation valves. Metal-seated DN1200 gate valves constructed from ASTM A216 WCB ensure fire-safe, thermal-expansion-resistant operation under continuous thermal cycling.
Cross-Country Oil & Gas Pipelines
Full-bore slab gate valves in NPS 48 / Class 300 allow smooth passage of intelligent pipeline pigs while providing robust double block and bleed security at sectionalizing valve stations.
Future Technological Trends in Large-Bore Gate Valves (2025–2035)
How digital diagnostics, advanced material science, and automated manufacturing are revolutionizing heavy fluid infrastructure.
IoT-Integrated Smart Valve Monitoring
Next-generation DN1200 valves incorporate embedded piezoresistive pressure sensors, acoustic leak-detection arrays, and stem vibration monitors connected to SCADA networks for predictive maintenance.
Zero-Fugitive-Emission Stem Seals
Meeting ISO 15848-1 Class AH requirements through live-loaded PTFE/Graphite packing sets and dual O-ring seal cartridges, preventing greenhouse gas and volatile chemical escape.
Additive Overlays & Nano-Coatings
Laser cladding of tungsten carbide and stellite alloys onto gate wedge contact faces increases cycle life 3-fold in erosive slurry and high-velocity water applications.
Wholesale DN1200 Gate Valve Procurement Q&A
In-depth answers to common engineering, commercial, and logistical inquiries raised by EPC project engineers and wholesale buyers.