High-Performance Butt Welded Fittings & Flanges
Explore our flagship series of heavy-wall butt weld elbows, equal and reducing tees, seamless reducers, and high-pressure ASME B16.5 flanges engineered for ultra-critical pressure piping networks.
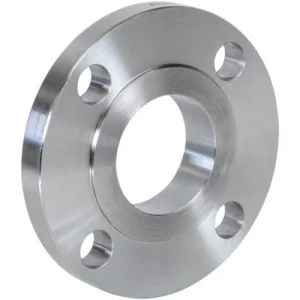
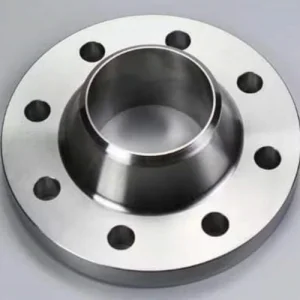
1. Industrial Metallurgy: High-Quality Butt Welded Components Engineering
In modern fluid mechanical processing, energy infrastructure, and chemical refineries, Butt Welded (BW) pipe fittings and flanges form the absolute backbone of continuous, leak-proof pressure containment. Unlike socket weld or threaded connections—which suffer from crevices prone to local stress concentration and crevice corrosion—a properly executed butt-welded joint yields a smooth, continuous volumetric connection. This monolithic metallic continuity optimizes fluid dynamics by reducing turbulence, minimizing pressure drop, and eliminating fatigue-inducing vibration points under cyclic thermal loads.
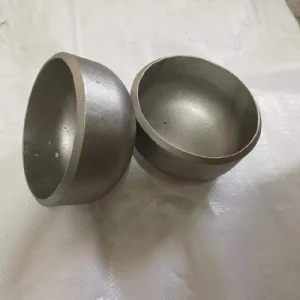
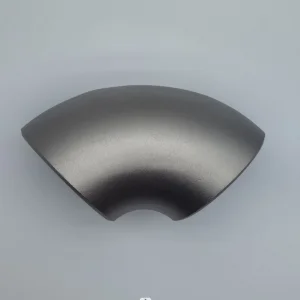
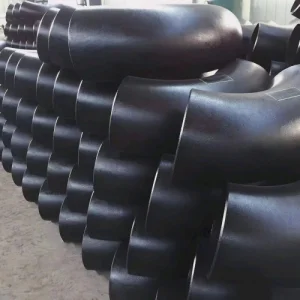
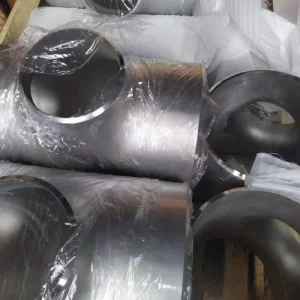
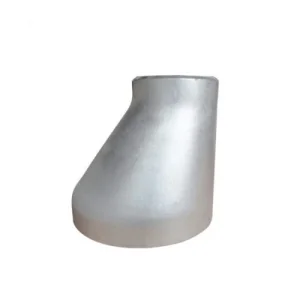
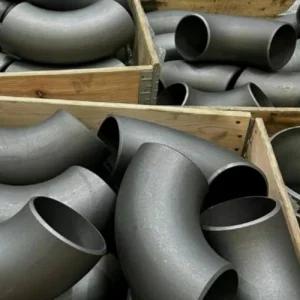
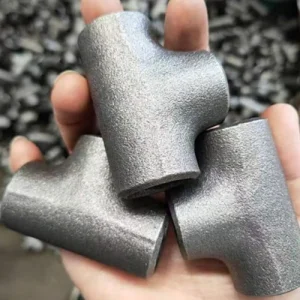
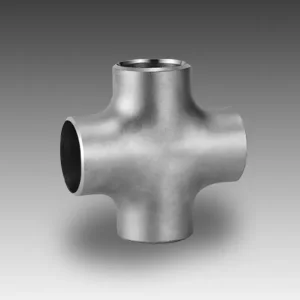
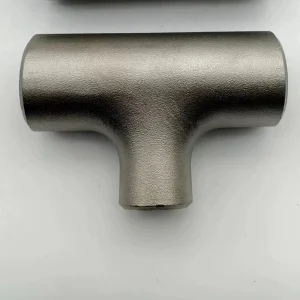
At Hebei Cangrun Pipeline Equipment Co., Ltd., manufacturing high-quality butt-welded fittings (including 45°/90°/180° long/short radius elbows, equal and reducing tees, concentric and eccentric reducers, and pipe caps) demands rigorous metallurgical control. We process premium grade raw carbon steel (ASTM A234 WPB, WPC), alloy steels (ASTM A234 WP11, WP22, WP91 for high-temperature steam services), stainless steels (ASTM A403 WP304/304L, WP316/316L, 317L, 310S), and duplex/super-duplex grades (UNS S31803, S32750). Every component undergoes precision end beveling according to ASME B16.25, establishing exact root faces, land dimensions, and bevel angles (37.5° ± 2.5°) essential for defect-free full-penetration field welding.
2. Global Commercial & Industrial Landscape
The worldwide industrial piping sector is undergoing a massive transformation driven by the global energy transition, LNG regasification expansions, offshore deepwater exploration, and modernizing aging power infrastructure across North America, Europe, and the Middle East. High-pressure piping systems operate under severe environmental conditions ranging from sub-zero cryogenic temperatures (-196°C) in LNG liquefaction plants to elevated thermal regimes (>600°C) in ultra-supercritical power boilers.
Energy Infrastructure & LNG
Surging demand for natural gas transmission requires high-strength low-alloy (HSLA) steel fittings such as MSS SP-75 WPHY 52, WPHY 60, and WPHY 65. These fittings must demonstrate high yield strength combined with guaranteed Charpy V-Notch impact toughness down to -46°C.
Petrochemical & Refining
Modern cracking units operate under aggressive hydrogen attack (HTHA) and sour gas environments. Sour service compliance per NACE MR0175/ISO 15156 dictates strict hardness caps (HRC ≤ 22) and tight control over carbon equivalent (CE) values during manufacturing.
Nuclear & Supercritical Steam
Boiler main steam lines demand specialized martensitic alloy fittings (ASTM A234 WP91/WP92) capable of resisting creep rupture at extreme temperatures. High-quality butt welding ensures thermal fatigue immunity over multi-decade service lifespans.
3. Mission-Critical Localized Application Scenarios
Industrial butt-welded piping components are customized for micro-environments where mechanical integrity cannot be compromised. Below are the key field deployment scenarios where Cangrun pipeline products deliver verified reliability:
| Application Domain | Primary Component Specified | Material Grade & Standard | Key Operational Challenge Solved |
|---|---|---|---|
| Subsea Risers & Manifolds | Heavy Wall WNRF Flanges & 5D Bends | Duplex UNS S31803 / Super Duplex S32750 | Resists severe chloride pitting corrosion, sulfide stress cracking (SSC), and high wave-fatigue forces. |
| Cryogenic LNG Terminals | Seamless Long Radius 1.5D Elbows | ASTM A403 WP316L / ASTM A860 WPHY 60 | Prevents brittle fracture transition down to -196°C; maintains microstructural grain ductility under thermal shock. |
| Hydrogen Transport Lines | Concentric / Eccentric Reducers & Caps | 316L Stainless (Ni content > 12%) / Low CE Steel | Eliminates hydrogen embrittlement pathways by controlling delta-ferrite levels and micro-void formation in weld seams. |
| Refining Hydrocracker Units | High Pressure Equal & Reducing Tees | ASTM A234 WP91 / WP22 Class 2 | Resists High-Temperature Hydrogen Attack (HTHA) and maintains yield strength under severe cyclic stress at 580°C. |
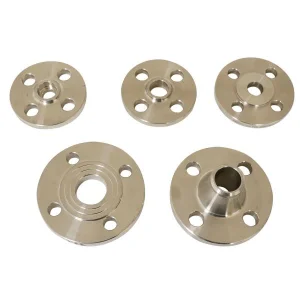
| High-Pressure Chemical Loop | ASME B16.5 Class 1500 Weld Neck Flanges | ASTM A105N / ASTM A182 F316L | Ensures zero fugitive emissions across gasketed joints through precision serrated spiral raised-face machining (Ra 3.2–6.3 µm). |
4. China Factory Supply Chain Resilience & Efficiency Advantages
Situated in Cangzhou, Hebei Province—the epicenter of China's industrial steel pipeline manufacturing hub—Hebei Cangrun Pipeline Equipment Co., Ltd. capitalizes on unprecedented supply chain integration. Our advanced manufacturing ecosystem transforms raw steel billets into fully tested, packaged, and certified butt-welded components with unmatched speed and economic efficiency.
Vertical Integration & Raw Material Synergy
Our three group factories (including Cangzhou Feiwo Metal Products Co., Ltd. and Cangzhou Feixiang Metal Products Co., Ltd.) enjoy direct, strategic partnerships with top-tier steel mills (such as Baosteel, TPCO, and Shougang). This integration guarantees priority sourcing of fully trace-analyzed, vacuum-degassed steel billets. By eliminating intermediary material markups, we deliver factory-direct cost savings straight to EPC contractors and international distributors.
High-Capacity Forming & Fast-Track Lead Times
Equipped with 5,000-ton hydraulic forging presses, automated hot-pushing elbow machines, cold-forming tee equipment, and CNC vertical lathes, our facilities handle seamless fittings up to 24 inches (DN600) and welded fittings up to 78 inches (DN1900) with wall thicknesses reaching 150 mm. Our streamlined production scheduling reduces standard manufacturing lead times by 35% compared to European or Western suppliers.
5. Manufacturing Technology Roadmap & Future Outlook
To maintain leadership in the high-spec industrial market, Cangrun Pipeline continuously upgrades its manufacturing technology roadmap. We combine traditional forging mastery with modern AI-driven manufacturing and digital quality monitoring tools:
Smart Hydro-Forming & Simulation
Utilizing finite element analysis (FEA) soft-modeling, we optimize wall thinning rates during hot pushing and cold extrusion of tees and elbows. This guarantees uniform wall thickness throughout the intrados and extrados regions, exceeding ASME B16.9 minimum tolerance requirements.
AI-Driven NDT Inspection
Integrating automated Digital Radiography (DR) and Phased Array Ultrasonic Testing (PAUT) algorithms, our quality line detects microscopic volumetric defects down to 0.1 mm, eliminating human visual error during weld seam qualification.
Real-Time Laser Cladding
For extreme corrosive services, we deploy laser cladding technology to apply high-nickel alloys (Inconel 625, Hastelloy C276) onto carbon steel flange faces and internal elbow bores, delivering solid-alloy corrosion protection at a fraction of solid duplex costs.
6. Global Localization Support & Compliance Guarantee
Executing international piping projects requires absolute compliance with regional standards and global engineering specifications. Cangrun Pipeline provides complete documentation, third-party inspection access, and localized logistics management for hassle-free port delivery worldwide.
Certifications & Material Traceability
Every product batch is issued with an EN 10204 3.1 or 3.2 Material Test Certificate (MTC) detailing chemical heat analysis, mechanical tensile strength, yield point, elongation, hardness, microstructural grain size, and impact test values. Our manufacturing plant operates under ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, and European Pressure Equipment Directive (PED 2014/68/EU CE stamp) standards.
Third-Party Inspection & Field Support
We routinely host third-party inspection agencies—including SGS, BV (Bureau Veritas), TUV, DNV, and Intertek—for hold-point visual inspection, dimensional verification, hydro-testing, and witnessing NDT procedures. Our dedicated export logistics desk manages ocean freight, customs clearances, and anti-dumping tariff optimization for destinations across Europe, North America, Southeast Asia, and the Middle East.
7. Technical FAQ: Expert Piping Engineering Insights
Answers to critical questions asked by procurement leads, piping stress engineers, and quality assurance inspectors when selecting butt-welded fittings and industrial flanges:
Additional Heavy-Duty Pipe Components
Browse further specialized pipeline equipment manufactured in our Cangzhou plants, available with full MTR 3.1 certification and custom schedule customization.