
Featured Pipe End Cap Solutions for French Engineering Projects
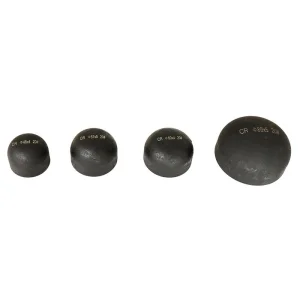
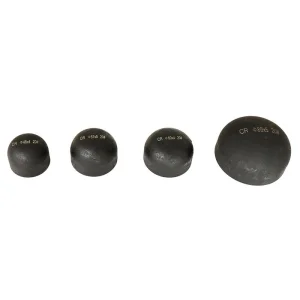
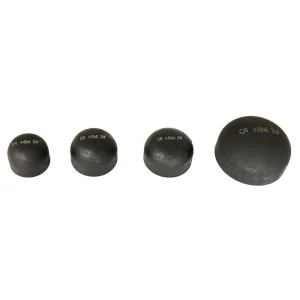
Direct factory supply of high-precision butt-weld, threaded, and sanitary caps fully compliant with ASME B16.9, EN 10253-2, and European Pressure Equipment Directive (PED 2014/68/EU).
France’s Industrial Renaissance: Demand Drivers for Certified Piping Components
France is undergoing a historical re-industrialization phase, anchored by its National Low-Carbon Strategy (SNBC), nuclear energy expansion (EPR2 initiative), and major investments in green hydrogen corridors.
The French industrial sector requires strict adherence to European norms (EN 10253-2, CODAP 2020) and international standards (ASME B16.9). From the chemical hubs in Normandy and the Rhône Valley to the offshore LNG terminals in Dunkirk and Marseille-Fos, engineering procurement teams face heightened scrutiny regarding material traceability, pressure safety margins, and localized compliance under the European Pressure Equipment Directive (PED 2014/68/EU).
Our engineering facility delivers precision-formed carbon steel, alloy, and stainless steel pipe caps designed specifically to handle extreme pressure cycles, cryogenic fluid storage, and severe corrosive environments common across French industrial ecosystems.
Critical Standards for French Compliance
- ✔️ PED 2014/68/EU Annex I: Essential safety requirements for pressure equipment operating above 0.5 bar.
- ✔️ CODAP 2020: French Code for Construction of Unfired Pressure Vessels.
- ✔️ RCC-M Code: Design and construction rules for mechanical components of PWR nuclear islands (EDF projects).
- ✔️ EN 10253-2 / EN 10253-4: European non-alloy and stainless steel butt-welding fittings specs.
- ✔️ EN 10204 Type 3.1 / 3.2: Full chemical & mechanical material certification with raw heat traceability.
Comprehensive Specification & Material Grade Matrix
Selecting the correct cap geometry and alloy chemistry is vital to preventing stress corrosion cracking, hydrogen embrittlement, and thermal fatigue in process piping.
| Material Category | Standard Equivalents (ASME / EN) | Wall Thickness Range | Primary French Application Scenarios | Key Testing Protocols |
|---|---|---|---|---|
| Carbon Steel | ASTM A234 WPB, WPC EN 10253-2 P235GH / P265GH |
SCH 10 to SCH 160 / XXS (Up to 150 mm) |
District heating (CPCU Paris), natural gas pipelines (GRTgaz), refinery utility lines. | Hydrostatic testing, UT wall thickness check, Charpy V-Notch (-20°C). |
| Austenitic Stainless | ASTM A403 WP304/304L, WP316/316L EN 10253-4 X2CrNiMo17-12-2 |
SCH 5S to SCH 80S | Chemical processing (Lyon Chemical Valley), wine storage (Bordeaux/Burgundy), pharmaceutical reactors. | PMI chemical verification, Intergranular Corrosion Test (ASTM A262 Practice E). |
| Low-Alloy Steel | ASTM A234 WP11, WP22, WP91 EN 10253-2 13CrMo4-5, 10CrMo9-10 |
SCH 40 to SCH XXS | High-pressure superheated steam loops, thermal power generation, hydrogen synthesis plants. | High-temperature tensile test, Hardness testing (HBW/HV), Magnetic Particle Inspection (MPI). |
| Duplex / Super Duplex | ASTM A815 UNS S31803 (2205) UNS S32750 (2507) |
SCH 10S to SCH 80S | Offshore platforms (Biscay Bay), desalination units, subsea brine containment lines. | Pitting Resistance Equivalent Number (PREN ≥ 40), Ferrite content analysis, RT 100%. |
Seamless Hot Forming
Produced using automated hydraulic pressing and deep-drawing dies without structural welds. Eliminates heat-affected zone (HAZ) vulnerabilities in high-stress pipeline end points.
Precision Beveling
Machined end bevels conform to ASME B16.25 and ISO 4200 standards (37.5° ± 2.5° with flat root land), enabling flawless root penetration during orbital or manual TIG welding.
Heat Treatment Protocols
All forged and formed caps undergo stress relief annealing, normalizing, or solution heat treatment in computer-controlled electric furnaces to restore optimal microstructural ductility.
Why French EPCs & Procurement Managers Choose Cangzhou Manufacturing Synergy
Situated in Hebei Province, our manufacturing matrix combines scale, raw material integration, and rigorous European quality assurance—delivering unprecedented value for French industrial buyers.
1. Direct Metallurgical Raw Material Access
By sourcing raw seamless tubes, plates, and round bars directly from Tier-1 state-owned steel conglomerates (Baosteel, TISCO, Shougang Group), our factory secures prime quality raw material at locked-in baseline costs. This insulation from spot market volatility translates into highly competitive, long-term fixed price quotes for European contractors managing multi-year infrastructure projects.
2. Advanced Hydraulic Forming Infrastructure
Our Cangzhou industrial park features high-capacity 5,000-ton hydraulic cold-pressing machines and hot-spinning dished head units capable of forming wall thicknesses up to 150 mm. Whether you require standard ASME B16.9 caps or custom toroidal dished ends for pressure vessels, our automated tooling setup guarantees dimensional tolerances within sub-millimeter margins.
Localized Application Scenarios Across French Industry
Tailored pipe end cap engineering solutions serving key economic corridors and specialized industries in France.
Nuclear Energy Systems (EDF Sites)
Locations: Flamanville, Gravelines, Penly
Secondary cooling circuits and non-safety piping loops demand high-integrity carbon (A234 WPB) and stainless steel caps. Subject to stringent RCC-M design rules, ultrasonic testing, and 100% radiographic weld inspections to prevent coolant leakage.
Green Hydrogen Networks (GRTgaz Projects)
Locations: Fos-sur-Mer, Le Havre Hydrogen Hubs
High-pressure gaseous hydrogen storage and transmission lines require low-carbon 316L or modified alloy pipe end caps resistant to atomic hydrogen penetration and embrittlement under operating pressures exceeding 200 bar.
Refining & Petrochemical Clusters
Locations: Etang de Berre, Normandy Refining Corridor
Heavy duty ASTM A234 WP11/WP22 alloy caps and ASME B16.9 carbon caps withstand severe catalytic cracking temperatures, hydro-desulfurization atmospheres, and aggressive sulfur compounds.
Sanitary & Hygienic Agro-Food Processing
Locations: Brittany Dairy & Beverage Plants
Polished 316L stainless steel threaded end caps and dished tank heads manufactured with internal roughness Ra < 0.4 µm, ensuring complete CIP (Clean-in-Place) sterility and EHEDG hygienic compliance.
Municipal Water & Heating (CPCU Paris)
Locations: Greater Paris, Lyon Urban Area
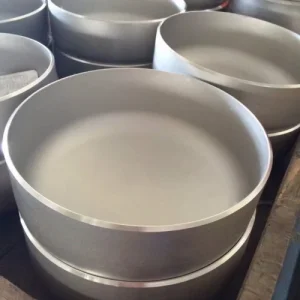
Large-diameter (DN600 to DN1200) carbon steel dished caps engineered for high-volume district steam and hot water loops, featuring anti-corrosion black primer or epoxy coatings.
Biopharmaceutical Cleanrooms
Locations: Île-de-France Biotech Parks
Electro-polished SUS316L caps and tri-clamp end closures designed for ultra-pure water (WFI) generation loops, guaranteeing zero product contamination and full material lot traceability.
Streamlined Logistics & Customs Fulfillment to France
We eliminate international procurement friction for French buyers through end-to-end logistics coordination and complete documentation packages.
Incoterms 2020 Flexibility (DDP / CIF / FOB)
Whether shipping directly to the Port of Le Havre, Port of Marseille-Fos, or inland project sites via DDP (Delivered Duty Paid), our export logistics department manages all customs clearing formalities.
Export Packaging & Seaworthy Protection
All caps feature plastic end bevel protectors, rust-inhibiting varnish or oil coating, and are packed into ISPM-15 compliant fumigated wooden crates or steel-banded pallets.
3rd-Party Witness Inspection (TÜV / BV / SGS)
We regularly coordinate with independent inspection agencies such as TÜV Rheinland, Bureau Veritas, or SGS to perform pre-shipment dimensional, NDT, and hydro-test verifications.
Request a Customized Tender Quotation
Provide your pipe schedule, wall thickness, material grade, and standard requirements. Our technical sales engineers respond within 24 hours with itemized pricing, technical data sheets, and estimated delivery schedules.
Send Inquiry NowFrequently Asked Questions for French Procurement Engineers
Expert answers regarding standards compliance, material equivalencies, testing procedures, and customs clearance.
How do ASME B16.9 cap wall thicknesses convert to European EN 10253-2 schedules?
ASME B16.9 specifies nominal pipe sizes (NPS) and schedules (e.g., SCH 40, SCH 80, STD, XS). EN 10253-2 uses outside diameter (OD) and wall thickness (T) in millimeters (e.g., Type A or Type B fittings). Our technical engineering team provides exact cross-reference mapping matrices to ensure that imported ASME caps precisely match existing EN metric piping dimensions in French facilities without creating internal flow restrictions or welding step-discontinuities.
Are your steel pipe caps fully compliant with the European Pressure Equipment Directive (PED 2014/68/EU)?
Yes. All pressure-retaining pipe caps destined for the French and broader EU market are manufactured under a certified Quality Assurance System conforming to PED 2014/68/EU Annex I requirements. Each delivery is accompanied by an EN 10204 Type 3.1 Material Test Certificate (MTC) detailing heat numbers, chemical ladle analysis, mechanical tensile/yield test results, impact values at sub-zero temperatures, and non-destructive test (NDT) reports.
What non-destructive testing (NDT) options are conducted on high-pressure dished caps?
Depending on project criticalities (such as high-pressure steam or hydrogen pipelines), we perform 100% Ultrasonic Testing (UT) for laminar defect detection in raw plate material, Magnetic Particle Inspection (MPI) or Liquid Penetrant Testing (LPT) for surface crack evaluation, Radiographic Testing (RT) on welded seams (if applicable), and Positive Material Identification (PMI) using XRF analyzers to guarantee alloy composition prior to dispatch.
Can you manufacture custom ellipsoidal or torispherical dished heads according to French CODAP rules?
Yes, our Cangzhou facility operates heavy hydraulic press tooling and spinning machinery to forge custom 2:1 ellipsoidal caps, torispherical heads (DIN 28011 / DIN 28013 equivalents), and hemispherical vessel closures according to customer drawings and CODAP structural thickness calculations.
What is the typical lead time for sea freight delivery from China to Port of Le Havre or Marseille-Fos?
Production lead time for standard ASME/EN pipe caps is typically 15 to 25 days depending on batch volume. Ocean transit time from Tianjin/Qingdao ports to Port of Le Havre or Marseille-Fos takes approximately 28 to 35 days. Express air freight options are available for emergency maintenance shutdowns (MRO).
Do you provide EN 10204 3.2 certificates witnessed by independent inspectors?
Yes. When requested by project specifications, we coordinate with accredited third-party inspection bodies (TÜV Rheinland, Bureau Veritas, DNV, SGS) to witness mechanical testing, non-destructive evaluations, and stamp EN 10204 3.2 certificates for nuclear or offshore installation compliance in France.
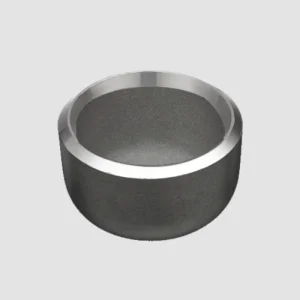
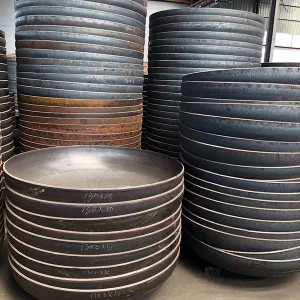
Full Line of Certified Cap & Fitting Products for European Projects
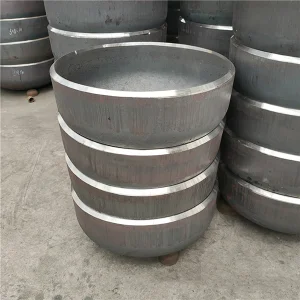
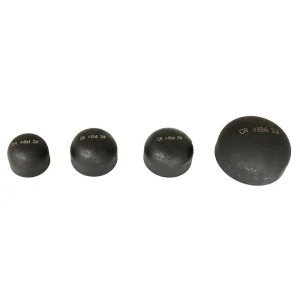
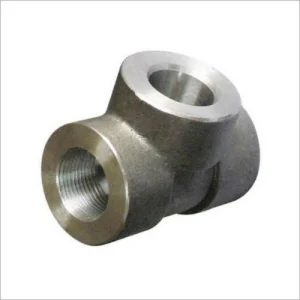
Browse our complete range of carbon, stainless, alloy, and forged thread pipe caps tailored to international engineering standards.
Accelerate Your Procurement for France Projects Today
Get direct-from-factory pricing, full PED 2014/68/EU compliance documentation, and comprehensive material certification within 24 hours.