
High-Performance Valves & Forged Fittings
Engineered for compliance with UK Water (WRAS), Offshore Energy (NACE MR0175), and High-Pressure Process Networks.
The UK Gate Valve Market: Industrial Context & Demand Drivers
Analyzing the strategic realignment of British fluid control systems across offshore energy, municipal water utilities, and green transition networks.
North Sea & Offshore Assets
The UK Continental Shelf (UKCS) demands extreme-reliability gate valves capable of surviving hostile marine environments. Legacy oil and gas infrastructure requires ongoing maintenance, life extension, and high-integrity isolation valves engineered to NACE MR0175 standards for sour oil service.
- Pressure Seal Bonnet Wedge Gate Valves for high-temperature steam injection
- Duplex 2205 & Super Duplex 2507 trims to prevent chloride stress corrosion cracking
- API 6D pipeline valves for offshore platform tie-backs and subsea manifolds
AMP8 Water Infrastructure Reform
Under Ofwat’s AMP8 regulatory framework (2025–2030), UK water authorities (e.g., Thames Water, Severn Trent, United Utilities) are committing billions in capital expenditure to modernize aging water networks, reduce leakage, and prevent storm overflow contamination.
- BS EN 1074-2 Resilient Seated Gate Valves with WRAS-approved EPDM wedges
- Non-Rising Stem (NRS) designs tailored for underground municipal distribution
- Zero-leakage bi-directional sealing to maintain clean water network pressure
Net Zero 2050 & Hydrogen Blending
The UK’s ambitious Net-Zero roadmap has spurred major investments in Carbon Capture, Utilization, and Storage (CCUS) projects (such as the East Coast Cluster and HyNet North West) alongside 20% hydrogen-blend natural gas pipeline trials.
- Fugitive emission control certified to ISO 15848-1 Class AH for hydrogen transport
- High-pressure forged steel gate valves designed for dense-phase CO2 handling
- Fire-safe testing validation in accordance with API 607 / ISO 10497
Technical Roadmap: Next-Generation Valve Manufacturing
Emerging technology vectors elevating structural performance, leakage prevention, and digital intelligence across critical fluid networks.
Zero-Emission Stem Sealing & Metallurgy
Fugitive volatile organic compound (VOC) leaks account for up to 60% of fugitive plant emissions. High-performance UK gate valves now deploy multi-stage stem packing systems combined with live-loaded Belleville spring washers to compensate for thermal cycling.
- Graphite Packing Systems: High-density expanded graphite rings with anti-extrusion braided carbon fibers.
- Hardfacing Trims: Stellite 6 overlay on solid wedge seats to prevent galling under high differential pressure (DP).
- Corrosion Resistance: NACE MR0175 compliant stem metallurgy (Inconel 718 or Nitronic 50) for harsh sour gas lines.
Smart Actuation & IIoT Digital Twin Integration
UK industrial sites are rapidly adopting smart, connected valves. By embedding non-intrusive sensor arrays within gate valve bonnet structures, asset managers can monitor stem stress, seat degradation, and operating cycles in real-time.
- Partial Stroke Testing (PST): Automated diagnostic cycling to verify emergency shutdown readiness without interrupting flow.
- Acoustic Leak Detection: Integrated piezoelectric sensors capable of identifying microscopic internal seat bypass.
- Modbus & HART Connectivity: Direct telemetry linking to SCADA platforms for predictive maintenance scheduling.
Comprehensive Macro Industry Solutions
Tailored valve configuration architectures matching the specific operational stresses of primary UK industrial applications.
| Industry Sector | Typical Valve Configuration | Standard Compliance | Material Specification | Key Performance Feature |
|---|---|---|---|---|
| Municipal Water Infrastructure | Resilient Seated Gate Valve (Z45X Series) | BS EN 1074-2, WRAS Approved | Ductile Iron EN-GJS-500-7, EPDM Coated Wedge | Full bore design, zero pressure drop, smooth flow channel preventing debris buildup |
| Offshore Oil & Gas / Refinery | Flexible Wedge OS&Y Gate Valve (API 600) | BS EN ISO 10434, NACE MR0175 | Forged ASTM A105N / A182 F316, Stellite 6 Trim | Heavy-duty rising stem, bolted bonnet, anti-blowout stem design with emergency grease injection |
| High-Pressure Power & Steam | Pressure Seal Bonnet Gate Valve | ASME B16.34, BS EN 12516 | Cast Alloy Steel ASTM A217 WC9 / C12A (P91) | Internal pressure dynamic sealing—higher fluid pressure increases bonnet seal integrity |
| Chemical Processing | Solid Wedge Stainless Gate Valve (Z41W) | BS EN 1984, PED 2014/68/EU | Austenitic Stainless Steel ASTM A351 CF8M / CF3M | Superior acid/alkali resistance, TA-Luft compliant packing, smooth micro-polished stem finish |
Need Custom Valve Specifications for UK Projects?
Consult with our lead engineering team for material selection, CAD drawings, and compliance documentation.
Localized UK Compliance & Standards Assurance
Ensuring frictionless UK import compliance, regulatory approval, and site-level integration.
UKCA & Pressure Equipment Regulations (PER)
Post-Brexit compliance demands clear validation under the UK’s Pressure Equipment Safety Regulations (PER 2016) alongside traditional European PED 2014/68/EU mandates. All pressure-retaining components are subjected to Module H/H1 conformity assessments.
BS EN 12266-1 Hydrostatic & Pneumatic Testing
Every gate valve unit shipped to the UK undergoes rigorous shell proof testing at 1.5x nominal pressure rating and seat tightness testing at 1.1x nominal pressure in strict compliance with BS EN 12266-1 Rate A (Zero Visible Leakage).
Traceable EN 10204 3.1 & 3.2 Certification
Material traceability is non-negotiable for UK high-hazard installations. Complete Material Test Reports (MTRs) detailing heat code numbers, chemical ladle analysis, mechanical tensile/impact testing, and 3rd party inspection sign-offs (DNV/Lloyd's Register) are provided with every batch.
China Industry 4.0 Factory: Supply Chain Resilience & Cost Optimization
Combining Cangzhou's advanced metallurgy cluster scale with British engineering precision to deliver cost-optimized, uncompromised piping solutions.
Automated Precision Foundry & Machining Scale
Operating across multiple state-of-the-art production bases in Cangzhou, Hebei, our manufacturing ecosystem integrates automated resin-sand casting molds, multi-axis CNC machining centers, and automated hard-facing robotic welding cells. By controlling the raw material foundry, forging hammers, and final hydrostatic testing in-house, we eliminate intermediate supply chain markups while strictly maintaining geometric tolerances (BS EN ISO 286).
- High-Throughput Casting: Capability to manufacture gate valves up to DN2400 (96 inches) and forged flanges up to DN4000.
- Integrated Metallurgical Lab: Optical emission spectrometers, Charpy V-notch impact testers, and Brinell hardness testing.
- Streamlined UK Freight Logistics: Rapid container consolidation and direct sea-freight routes from Tianjin / Qingdao port directly to Felixstowe, Southampton, and Liverpool ports.
Supply Chain Performance Snapshot
Global Enterprise Procurement & Vendor Qualification Guide
A structured framework for UK procurement teams and EPC contractors evaluating international valve and fitting original equipment manufacturers (OEMs).
1. Material Verification & MTR Audit
Always mandate EN 10204 Type 3.1 inspection certificates. Cross-check heat numbers stamped on valve bodies with chemical spectrometry analyses to guarantee carbon equivalent (CE) limits for weldability.
2. Non-Destructive Examination (NDE)
For critical isolation duties in high-pressure or toxic service, specify Radiographic Testing (RT) on casting critical areas per ASME B16.34 Appendix-I and Positive Material Identification (PMI) on alloy trims.
3. Factory Acceptance Testing (FAT)
Utilize qualified independent inspectors (e.g., TUV, Bureau Veritas, SGS) to witness high-pressure gas body testing, low-pressure seat pneumatic testing, and torque output measurements under max differential pressure.
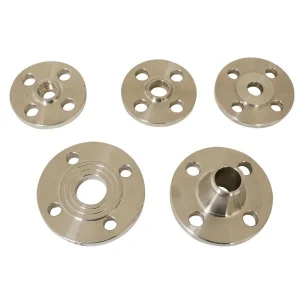
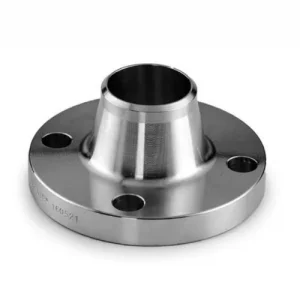
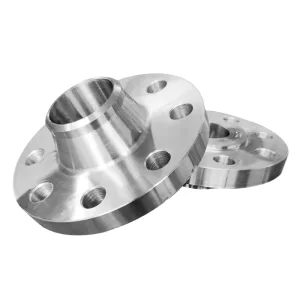
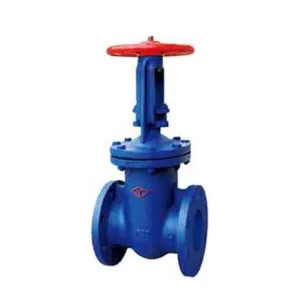
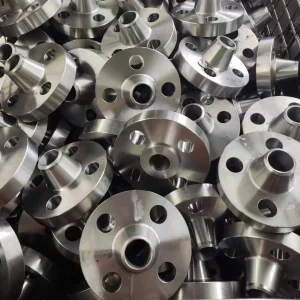
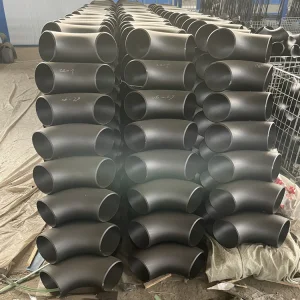
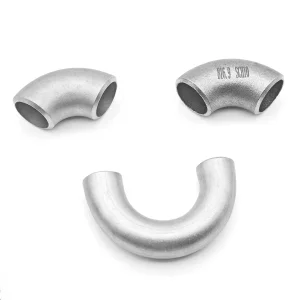
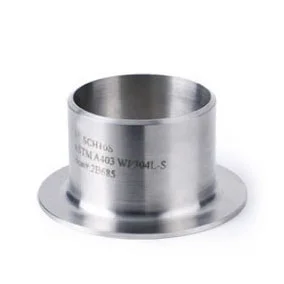
Industrial Flanges, Valves & Pipe Fittings for UK Infrastructure
Explore our complete manufacturing line built for seamless compatibility with British Standards (BS), EN, and ASME piping schedules.
Frequently Asked Questions by UK Engineers & Procurement Managers
Expert insights covering standards, materials, pressure testing, and UK import compliance for industrial gate valves.
How do BS EN gate valve standards compare directly to American API standards?
BS EN standards (such as BS EN 1984 for steel gate valves and BS EN 1074 for water supply) closely align with API 600 / API 6D in terms of wall thickness and pressure-temperature ratings. However, face-to-face dimensions under BS EN 558 differ slightly from ASME B16.10 in select sizes. Our factory manufactures dual-standard body castings compatible with both ISO/EN and ASME flanged drillings to facilitate seamless replacement in existing UK plants.
What valve materials are required for North Sea sour gas (NACE) environments?
For offshore and refinery applications exposed to hydrogen sulfide (H2S), components must comply with NACE MR0175 / ISO 15156. This mandates strict control over maximum material hardness (typically <22 HRC for carbon steels like ASTM A105N or WCB) to prevent sulfide stress cracking (SSC). Stems are supplied in duplex stainless steels or Inconel 718, and all pressure-retaining welds undergo post-weld heat treatment (PWHT).
Are resilient seated gate valves suitable for UK potable water systems?
Yes. Resilient seated gate valves (Z45X design) feature an EPDM-encapsulated ductile iron wedge that yields zero-leakage isolation (BS EN 12266-1 Rate A). For UK municipal potable water networks, the internal elastomer must hold WRAS (Water Regulations Advisory Scheme) or BS 6920 approval to ensure no toxic leaching or biological growth occurs in drinking water.
What is the importance of ISO 15848-1 certification for UK Net Zero projects?
ISO 15848-1 specifies testing procedures for measuring fugitive emissions from industrial valves. In light of the UK’s Net Zero targets and strict Environment Agency regulations, chemical and energy plants require Class AH or BH certification (helium leak rate <10^-5 mg·s^-1·m^-1) to prevent greenhouse gas and VOC escape from the valve stem packing seal.
What documentation is delivered with custom OEM valve shipments to the UK?
Every shipment is backed by a comprehensive QA package including: EN 10204 3.1 Material Test Reports (chemical/mechanical analysis), Hydrostatic & Pneumatic Test Certificates, NDT Inspection Reports (UT/RT/PT), Pressure Equipment Regulations (PER) UKCA/CE Declaration of Conformity, and complete Operation & Maintenance (O&M) manuals in English.
How does your Cangzhou factory manage lead times and UK port delivery logistics?
By keeping extensive raw material stocks of standard forged bar and sand casting patterns for popular sizes (DN50 to DN600), standard gate valves ship within 15–20 days. Through integrated freight contracts, sea shipment from China directly to major UK hubs (Felixstowe, Southampton, Grangemouth) takes approximately 28 to 35 days, supported by complete customs clearance documentation.
Ready to Optimize Your UK Valve Supply Chain?
Get factory-direct quotes, technical datasheets, and compliance support for your upcoming pipeline tenders.