
Precision-Engineered Elbow Solutions for Kazakh Infrastructure
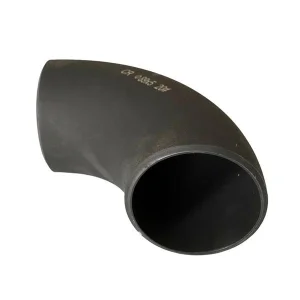
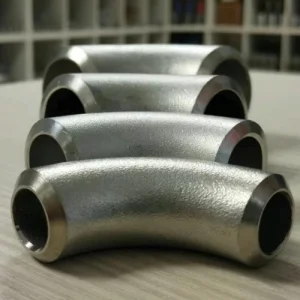
Featured high-pressure carbon steel and stainless steel pipe elbows designed for oil & gas transport, thermal power plants, and mining slurry systems across Kazakhstan.
Kazakhstan’s Industrial Evolution & Pipeline Component Demand
As the primary economic motor of Central Asia, the Republic of Kazakhstan stands at a pivotal intersection of global energy supply and regional infrastructure modernization. Driven by vast natural resource reserves in the Caspian Basin, massive industrial modernization agendas, and the strategic trans-Eurasian trade corridor (Middle Corridor), Kazakhstan’s reliance on robust, certified piping equipment has expanded exponentially over the last decade.
The operational environment in Kazakhstan presents unique engineering challenges. Pipeline infrastructure must survive extreme continental temperature variations—ranging from severe sub-zero winters dipping below -40°C in northern regions like Astana and Pavlodar to ambient summer temperatures exceeding +40°C in southern and western deserts. Furthermore, extracting sour crude oil and natural gas rich in Hydrogen Sulfide (H2S) and Carbon Dioxide (CO2) from mega-fields such as Tengiz, Kashagan, and Karachaganak demands ultra-reliable metallurgical integrity from every butt-weld elbow, tee, and reducer integrated into the system.
To support this high-stakes industrial ecosystem, international engineering, procurement, and construction (EPC) contractors require pipeline manufacturing partners capable of delivering double-certified products: bridging Western specifications (ASME/ANSI, EN, API) with Eurasian customs and safety frameworks (GOST, ST RK, EAC TR CU 032/2013 regulations).
Energy Sector Upgrades
Upstream expansion, gas compression stations, and refinery modernizations at Atyrau, Shymkent, and Pavlodar require high-yield carbon steel (WPHY52-WPHY70) and sour-service resistant seamless elbows.
Extreme Arctic Toughness
Low-temperature carbon steel (ASTM A420 WPL6) and specialized micro-alloyed steels formulated to maintain Charpy V-notch impact energy values down to -46°C to eliminate brittle fracture risks.
District Heating Networks
Decarbonization and rehabilitation of municipal Thermal Power Plants (CHP/ТЭЦ) demand large-diameter (up to DN1400) carbon steel elbows for high-pressure steam loops and urban heating lines.
Advanced Metallurgy & Material Selection Whitepaper
Selecting the precise steel grade and manufacturing methodology for pipe elbows directly governs system longevity, maintenance cycles, and plant safety. Our production facilities deploy advanced hot-push forming, cold extrusion, and heat treatment protocols to manufacture seamless and welded elbows tailored for Kazakhstan's severe-duty applications.
| Material Category | International Standard | GOST / ST RK Equivalent | Operational Temperature | Primary Industrial Applications |
|---|---|---|---|---|
| Standard Carbon Steel | ASTM A234 WPB / WPC | GOST 17375 Grade 20 | -29°C to +425°C | General utility lines, water transport, low-pressure gas distribution networks. |
| Low-Temp Carbon Steel | ASTM A420 WPL6 | GOST 17375 Grade 09G2S | -46°C to +345°C | Cross-country gas pipelines, northern district heating, uninsulated outdoor installations. |
| High-Yield Line Pipe Steel | MSS SP-75 WPHY 52 / 60 / 65 / 70 | GOST 30753 Grade 09G2S-12 | -40°C to +120°C | High-pressure transmission oil & gas trunk lines (CPC, Trans-Kazakhstan line). |
| Austenitic Stainless Steel | ASTM A403 WP304/304L / WP316/316L | GOST 5632 08Ch18N10T / 03Ch17N14M3 | -196°C to +650°C | Chemical processing plants, fertilizer complexes, acidic slurry handling, offshore duty. |
| Duplex & Super Duplex Steel | UNS S31803 (2205) / UNS S32750 (2507) | GOST 5632 02Ch22N5AM3 | -50°C to +300°C | High-chloride media, sour gas injection, high-pressure corrosive wellheads. |
Technical Focus: Sour Service & NACE Compliance
In fields with high H2S concentration (such as Kashagan and Tengiz), standard carbon steel elbows are susceptible to Hydrogen-Induced Cracking (HIC) and Stress Corrosion Cracking (SCC). We manufacture custom seamless elbows complying strictly with NACE MR0175 / ISO 15156. By controlling carbon equivalency (CEQ ≤ 0.43%), restricting sulfur content (S ≤ 0.002%), and performing specialized post-weld heat treatment (PWHT), our elbows deliver uncompromised structural integrity against sulfide stress cracking.
Standards Harmonization: Bridging ASME B16.9 and GOST 17375
A frequent challenge for procurement teams in Central Asia is reconciling Western engineering drawings (ASME B16.9) with Eurasian economic union regulatory frameworks (GOST / EAC). Our manufacturing engineering team provides full cross-referencing capabilities to ensure seamless technical acceptance by national safety authorities (Gostekhnadzor).
ASME / ANSI B16.9 Dimensional Norms
Factory-made wrought butt-welding fittings. Standardized center-to-end dimensions, long radius (1.5D) and short radius (1.0D) configurations. Pressure ratings mapped directly to pipe schedule (SCH 40, SCH 80, SCH 160, XXS).
GOST 17375-2001 & GOST 30753-2001
Eurasian standards for 3D (R≈1.5Dy) and 2D (R≈1.0Dy) seamless carbon and low-alloy steel elbows. Specified by outer diameter (DN in mm) and wall thickness, engineered for high wall-thickness ratio safety margins.
EAC TR CU 032/2013 Certification
Mandatory Technical Regulation of the Customs Union on safety of equipment operating under pressure. Our factory provides complete passport documentation, material test certificates (EN 10204 3.1 / 3.2), and EAC declarations.
Localized Application Scenarios in Kazakhstan
Our pipe elbows serve as critical flow control elements across Kazakhstan's core industrial sectors. Here is how our specialized production lines support local field operations:
1. Oil & Gas Trunk Lines & Refining
Used in crude oil gathering lines, gas compressor stations, and hydrocracker units in the Caspian region. Heavy wall seamless carbon steel 90° elbows (DN200 to DN1200) withstand high cyclic surge pressures and abrasive sand particles.
2. Mining, Metallurgy & Slurry Transport
Concentrator plants and hydrometallurgical complexes in Karaganda, East Kazakhstan, and Kostanay process iron ore, copper, and bauxite. We supply thick-walled abrasion-resistant ceramic-lined or hardened alloy elbows engineered for slurry abrasion.
3. Municipal & Industrial District Heating
Overhauling aging Soviet-era thermal networks requires high-volume supplies of pre-insulated steel elbows. Grade 09G2S low-alloy steel elbows provide superior weldability and fatigue resistance under seasonal thermal expansion stress.
Rigorous Factory Testing & Quality Verification
To ensure 100% operational reliability in harsh Central Asian climates, every elbow undergoes structured quality inspection throughout manufacturing. We enforce zero-defect quality control protocols from raw steel billet verification to final surface coating.
-
Chemical Analysis & PMI Testing
Optical Emission Spectrometry and Positive Material Identification (PMI) verify precise alloy contents, carbon equivalency (CEQ), and trace element thresholds prior to heat treating.
-
Sub-Zero Charpy V-Notch Impact Testing
Mechanical testing conducted at -40°C and -46°C verifies energy absorption capacity (minimum 27 Joules average), ensuring complete resistance against catastrophic low-temperature brittle fracture.
-
Non-Destructive Testing (NDT)
100% Ultrasonic Testing (UT) for wall thickness consistency and internal laminations, combined with Radiographic Testing (RT) on welded elbow seams, Magnetic Particle Inspection (MT), and Hydrostatic testing.
Logistics Architecture: Seamless Direct Delivery to Kazakhstan
Efficient freight delivery is essential for meeting EPC project milestones. Leveraging China's direct land rail connectivity with Kazakhstan, our export operations provide direct rail and overland truck transit solutions that bypass port congestion and reduce transit times.
Rail Freight via Khorgos / Alashankou
Direct block-train transport from main production hubs to Almaty-1/Almaty-2, Astana, Shymkent, and Karaganda stations, delivering typical transit windows of 10 to 14 days.
Heavy-Haul Truck Transport
For oversized items (up to DN2000 welded elbows) or urgent maintenance shutdowns, direct road freight via border crossing points (Dostyk/Khorgos) delivers door-to-door directly to the job site.
Export Packaging & Anti-Corrosion
All elbows are treated with black rust-preventive varnish, plastic end caps, and packaged in seaworthy wooden cases or heavy-duty steel crates to prevent mechanical damage during transit.
Future-Ready Technology Roadmap (2025–2030)
As Kazakhstan moves toward greener industrial initiatives and hydrogen energy blending projects, pipeline infrastructure demands are transitioning toward next-generation metallurgical engineering. Our facility is actively advancing several key technology initiatives:
- Hydrogen-Ready Elbow Manufacturing: Developing low-hardness, high-purity micro-alloyed carbon steel fittings engineered to resist hydrogen embrittlement in natural gas blending networks.
- Automated Hot-Push Induction Bending: Integrating real-time infrared temperature control during induction bending to optimize grain structure uniformity across long-radius elbows.
- 3D Laser Metrology & Beveling: Implementing automated robotic beveling systems to ensure perfect root face prep for automatic orbital field welding.
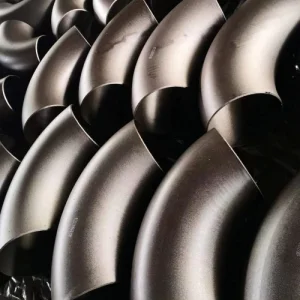
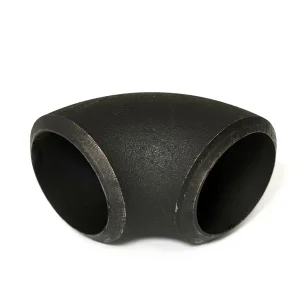
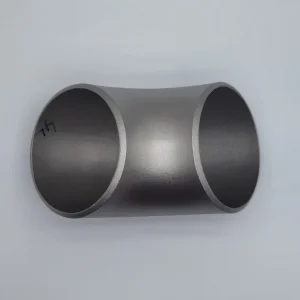
Complete Commercial Elbow Catalog for Kazakhstan Projects
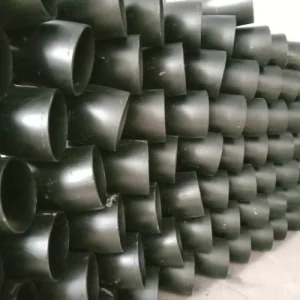
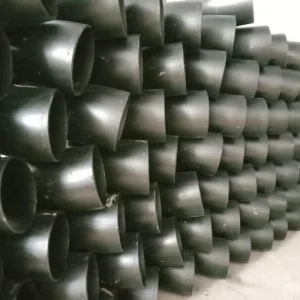
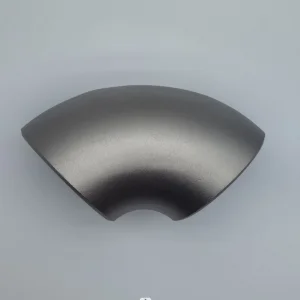
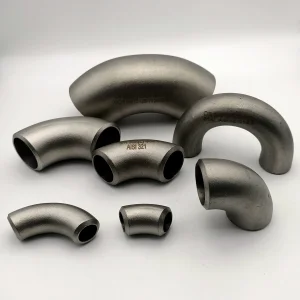
Explore our full range of certified carbon, stainless, and alloy steel butt-weld elbows available for direct export to Central Asian destinations.

Frequently Asked Questions (Procurement & Technical)
What certificates are provided for custom elbow shipments to Kazakhstan?
Every shipment is accompanied by Mill Test Certificates (MTC) according to EN 10204 3.1 or 3.2, full Chemical & Mechanical test reports, NDT (UT/RT) inspection certificates, heat treatment charts, and EAC TR CU 032/2013 conformity documentation required for customs clearance in Kazakhstan.
How do you guarantee impact strength for elbows installed in cold regions like Astana or Karaganda?
We utilize normalized or quenched-and-tempered low-alloy steels (such as ASTM A420 WPL6 or GOST 09G2S). We perform Charpy V-notch impact testing at -40°C or -46°C on every production heat code to verify minimum absorbed impact energy levels.
Can your factory manufacture elbows according to GOST 17375-2001 dimensions?
Yes. We operate dedicated tooling for GOST dimensions (outer diameter Dy and matching wall thickness metric series) as well as ASME B16.9 standards. We manufacture both 3D (R≈1.5Dy) and 2D (R≈1.0Dy) seamless elbows.
What is the typical rail freight transit time from your factory to Kazakhstan?
Direct rail container shipments departing through Alashankou / Khorgos gateways typically reach Almaty, Shymkent, or Astana station terminals within 10 to 14 days following customs clearance.
Do you offer third-party inspection (TPI) option before dispatch?
Absolutely. We regularly coordinate with international third-party inspection agencies including SGS, BV (Bureau Veritas), TUV, and DNV to perform visual, dimensional, material verification, and loading inspections at our works.
Partner with a Certified Elbow Manufacturer for Kazakhstan
Get engineering consultation, technical drawing confirmation, and direct factory quotation for your project schedule within 24 hours.
Send Inquiry Now