
Featured Industrial Fittings & Piping Components
High-precision manufactured carbon steel, alloy, stainless, and malleable pipeline products engineered for rigorous global industrial standards.
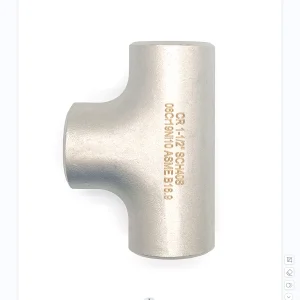
Best ANSI ASME B16.9 Carbon Steel Elbow Stainless Pipe Fitting Equal Tee
Precision butt-weld equal tees and elbows engineered for high-pressure fluid lines, oil refineries, and structural process piping networks.
View Product Details →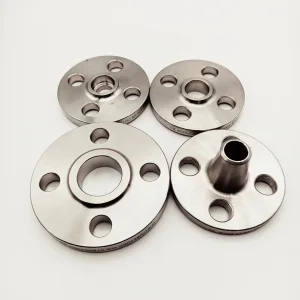
China ANSI B16.5/DIN/EN1092/GOST/BS Forged Pipe Flange Manufacturer
Comprehensive range of PN10/16 weld neck, blind, slip-on, and flat plate forged flanges for severe duty chemical processing.
View Product Details →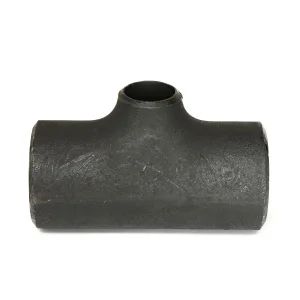
Wholesale Carbon Pipe Fittings of Equal/Straight/Reducing Tee ASTM
ASTM A234 WPB standard equal and reducing tees featuring seamless cold-drawn microstructures and full dimensional inspection.
View Product Details →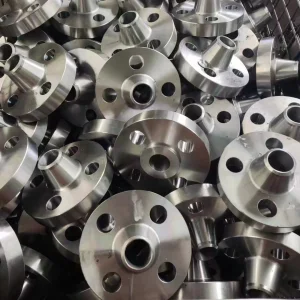
Famous High Pressure DIN 2638 DIN 2628 WN Flange PN160 PN250 A105
Ultra-high-pressure weld neck flanges (DN15–DN80) manufactured in A105 and S235JR for boiler plants and energy generation systems.
View Product Details →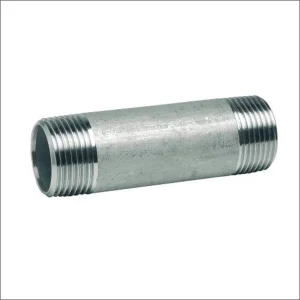
China Galvanized Steel & Stainless Steel Pipe Nipples Factory
Precision NPT and BSPT threaded steel pipe nipples with hot-dip zinc protective coatings for water supply and gas distribution line connections.
View Product Details →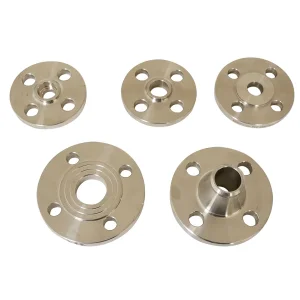
Wholesale High Pressure Orifice Flanges WN Flat Plate Blind DIN PN16
Precision-machined orifice flange assemblies designed for differential pressure measurement in chemical process lines.
View Product Details →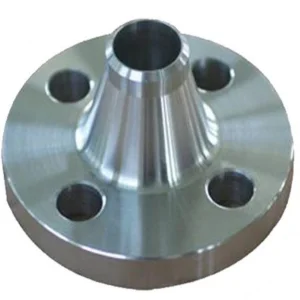
Discount Weld Neck Slip On Blind Flange Manufacturer & Supplier
Heavy-duty ASME/ANSI standard blind and slip-on flanges rated for high-stress industrial applications and offshore pipelines.
View Product Details →
China A105 Carbon Steel Flanges Manufacturers & Export Supplier
Forged ASTM A105 carbon steel flanges for high-temperature and ambient service in pressure systems and power facilities.
View Product Details →Metallurgical Fundamentals & Manufacturing Kinetics of Malleable Iron Pipe Fittings
An authoritative engineering analysis of Blackheart vs. Whiteheart cast iron, thermal annealing cycles, thread geometry, and mechanical performance limits under extreme industrial stress.
Blackheart Malleable Cast Iron (ASTM A197 / EN 1562 GJMB)
Blackheart malleable iron is produced via a non-decarburizing thermal annealing process in a neutral furnace atmosphere at 900°C–950°C. Fe3C cementite decomposes into irregular aggregates of temper carbon (nodular graphite clusters) embedded in a ductile ferrite matrix. This yields exceptional toughness, high elongation (>10%), and resistance to thermal shock in gas and fluid containment lines.
Whiteheart Malleable Cast Iron (EN 1562 GJMW)
Whiteheart malleable iron relies on a decarburizing heat treatment in an oxidizing environment at 980°C–1050°C. Carbon is burned off from the outer casting boundary, creating a low-carbon steel-like skin with a high-carbon core. Whiteheart fittings exhibit high surface hardness and superior weldability, making them ideal for specialized structural clamps and heavy-duty mechanical engineering joints.
Thread Precision & ASME B16.3 / ISO 7-1 Tolerance
To prevent spiral leak paths in threaded pipe systems, malleable iron fittings undergo automated CNC chamfering and tapping. NPT (National Pipe Taper) per ASME B16.3 features a 60° thread angle with a 1-in-16 taper, while BSPT (British Standard Pipe Taper) per ISO 7-1 utilizes a 55° thread angle. Precise pitch diameters guarantee bubble-tight metal-to-metal sealing under working pressures up to 25 bar (362 psi).
Metallurgical Benchmark: Malleable Iron vs. Alternative Piping Materials
When specifying pipeline components for municipal water, HVAC, fire protection, and gas distribution, procurement officers must balance mechanical strength, vibration damping, and cost-effectiveness. The matrix below contrasts ASTM A197 malleable iron against alternative metallurgy.
| Material Specification | Standard Reference | Tensile Strength (MPa) | Yield Strength (MPa) | Elongation (%) | Primary Industrial Advantage |
|---|---|---|---|---|---|
| Blackheart Malleable Iron | ASTM A197 / EN 10242 | 330 – 370 | 200 – 220 | 10 – 14 % | Exceptional threadability & fatigue resistance |
| Ductile Iron (Nodular Iron) | ASTM A536 / EN 1563 | 400 – 600 | 250 – 400 | 7 – 18 % | Superior tensile rating for large municipal mains |
| Gray Cast Iron | ASTM A48 / EN 1561 | 150 – 250 | None (Brittle) | < 0.8 % | Excellent vibration damping; strictly low-pressure gravity lines |
| Forged Carbon Steel | ASTM A105 / ASME B16.11 | 485 – 550 | 250 – 300 | 22 – 30 % | Extreme high-pressure refinery applications (Class 3000+) |
| Austenitic Stainless Steel | ASTM A403 WP304/316 | 515 – 620 | 205 – 240 | 35 – 45 % | Maximum chemical corrosion resistance for acid/pharmaceutical duty |
Global Market Dynamics & Procurement Optimization for Malleable Fittings
Analyzing worldwide demand trends, logistics risk mitigation, tariffs, and total cost of ownership (TCO) when sourcing from premier industrial clusters in China.
Regional Demand Shifts & Infrastructure Megatrends
The global demand for malleable iron pipe fittings is driven by rapid urban growth across North America, Europe, the Middle East, and Southeast Asia. Key growth vectors include:
- Commercial Fire Sprinkler Retrofits: Strict NFPA 13 and EN 12845 mandates requiring UL/FM certified 300 psi threaded malleable elbows and tees.
- HVAC & District Heating Expansion: High-density residential construction utilizing hot-dip galvanized fittings to prevent interior tuberculation and oxide buildup.
- Modular Prefabricated Plumbing Skids: Factory-built mechanical assemblies relying on standardized NPT/BSPT male and female iron unions.
Overcoming Freight Volatility & Supply Disruptions
International piping procurement requires strategic logistics planning. Experienced manufacturers such as Hebei Cangrun Pipeline Equipment Co., Ltd. offer complete shipping risk mitigation:
- Cangzhou Logistics Hub Advantage: Proximity to Tianjin (Xingang) Port reduces inland transport overhead and enables rapid container loading cycles.
- Container Palletization Engineering: Wooden pallets with anti-rust VCI shrink wrap to eliminate marine salt-air oxidation during trans-oceanic transit.
- Transparent Surcharge Hedging: Real-time freight tracking and proactive ocean carrier routing around high-density port bottlenecks.
Localized Application Scenarios & Heavy Industry Use-Cases
From municipal fire protection networks to complex refinery process piping, malleable iron fittings provide the optimal balance of mechanical strength and leak-tight joint reliability.
1. Automatic Fire Protection Sprinkler Systems
Threaded malleable iron 90° elbows, tees, and cross fittings are the gold standard for branch lines in commercial wet and dry fire sprinkler systems. Rated for 300 psi (2.07 MPa) working pressure per UL/FM safety guidelines, their high yield strength absorbs water hammer shocks during sudden valve actuation.
2. Compressed Air & Industrial Gas Distribution
Factory air header loops require complete pressure integrity. Black finish ASTM A197 malleable iron fittings with clean NPT threads bonded with anaerobic thread sealant guarantee zero gas leakage. They handle high vibration from reciprocating air compressors without thread loosening or micro-cracking.
3. Potable Water Plumbing & HVAC Circulation
Hot-dip galvanized malleable fittings conforming to ISO 49 / EN 10242 feature high-purity lead-free zinc coatings (>500 g/m²). They resist aggressive tap water chemistry, prevent galvanic corrosion, and carry NSF/ANSI 61 and WRAS drinking water health approvals.
4. Oil & Fuel Transfer Pipelines
Black iron malleable unions with brass-to-iron ground joints (ASME B16.39) provide positive metal-to-metal seating for hydrocarbon line connections. Capable of repeated disassembly for maintenance without compromising pressure seal integrity.
5. Modular Structural Pipe Railing & Key Clamps
Whiteheart malleable iron structural clamps allow quick slip-on construction of safety handrails, pedestrian barriers, and storage racks without welding. High tensile resistance prevents joint shear under dynamic impact loads.
6. Agricultural Irrigation & Fertigation Networks
Malleable reducing bushings, couplings, and street elbows provide seamless branch downsizing in high-flow agricultural pumping stations, resisting mechanical damage from tractor movement and soil shifting.
Global Compliance Standard & Engineering Quality Verification
Rigorous mill test procedures, non-destructive testing (NDT), and international certification frameworks governing Cangzhou manufacturing excellence.
100% Submerged Air Pressure Testing
Every single malleable iron fitting manufactured under our ISO 9001 quality program undergoes pneumatic pressure testing at a minimum of 0.6 MPa (87 psi) while fully submerged in liquid tanks. Any casting micro-porosity, pinhole, or thread defect produces visible bubbles, resulting in immediate rejection. For heavy-duty Class 300 series, hydrostatic proof testing is executed at 1.5 times working pressure rating.
Spectrometric & Metallographic Inspection
Raw pig iron, scrap steel, and alloy additions are verified via direct-reading optical emission spectrometers prior to furnace tapping. Following the long annealing cycle, metallographic micro-sections are evaluated under optical microscopes to verify complete cementite breakdown into temper carbon nodules without free iron carbides that could cause brittleness.
Technology Roadmap: Next-Generation Manufacturing & Eco-Galvanizing
Pioneering smart foundry automation, AI optical thread sorting, and zero-emission thermal annealing kinetics for sustainable pipeline infrastructure.
AI Optical Laser Thread Inspection
Replacing manual plug gages with high-speed 3D laser scanners on CNC production lines. Automated algorithms verify thread pitch, flank angle, chamfer depth, and taper angle within 5 micrometers in under 0.8 seconds per fitting.
Low-Lead & Trivalent Hot-Dip Zinc Baths
Innovating environmental hot-dip galvanizing technology that completely eliminates lead additions from molten zinc kettles, ensuring full compliance with upcoming EU REACH and US EPA potable water purity standards.
Digital Twin Furnace Annealing Control
Integrating IoT thermal sensors throughout continuous annealing tunnel kilns. Real-time temperature optimization algorithms dynamically adjust heating zones to minimize energy consumption while guaranteeing 100% graphite nodulization.
How to Evaluate Malleable Iron Pipe Fitting Manufacturers & Companies
Essential vendor pre-qualification criteria for EPC contractors, wholesale distributors, and engineering procurement heads when auditing Chinese pipe fitting factories.
1. Vertical Foundry Integration
Verify whether the manufacturer operates its own electric induction melting furnaces and continuous annealing kilns. Direct source foundries offer superior batch-to-batch chemical control compared to secondary machine shops buying raw black castings from third parties.
2. Threading Tooling & Gauge Calibration
Ensure the supplier uses automated multi-axis CNC tapping equipment with hardened tungsten carbide taps. Inquire about working plug gauge calibration intervals per ASME B1.20.1 to avoid site assembly thread jamming.
3. Galvanizing Weight & Adhesion Standards
Request mill verification of zinc coating mass per ISO 1461 or ASTM A153. Premium hot-dip fittings should exceed 500 g/m² (approx. 70 microns) and pass magnetic thickness testing as well as knife-edge peel tests for coating integrity.
Industrial Valves, Caps, Bends & Flange Series
Complete your pipeline bill of materials with certified companion fittings, high-pressure caps, and industrial flow control valves.
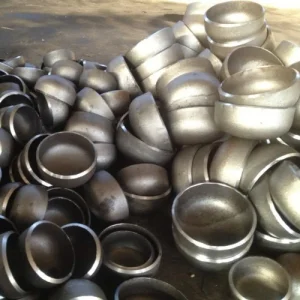
Discount Steel Pipe Cap Manufacturer & Factory Service
Heavy-duty butt-weld end caps in carbon and stainless steel for pipe line termination and pressure vessel headers.
View Product Details →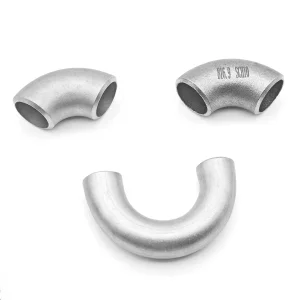
Buy High Quality 45/90-Degree Elbow Stainless & Carbon Steel Fittings
Long and short radius 45° and 90° elbows manufactured to ASME B16.9 standards for seamless flow deflection.
View Product Details →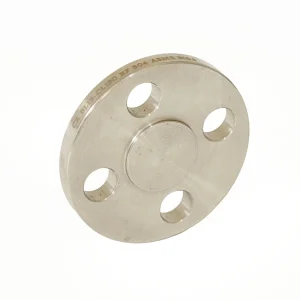
Discount GOST 12820-80 12821-80 Steel Flange Manufacturers
Russian GOST standard flat plate and weld neck steel flanges tailored for Eastern European and Central Asian pipeline contracts.
View Product Details →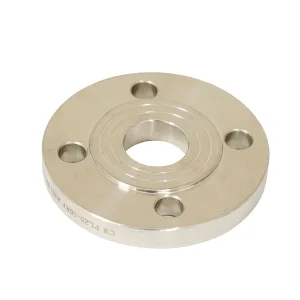
China Carbon Steel Flanges Manufacturers & Engineering Service
Comprehensive range of forged carbon steel flanges produced under strict ISO 9001 quality audit parameters.
View Product Details →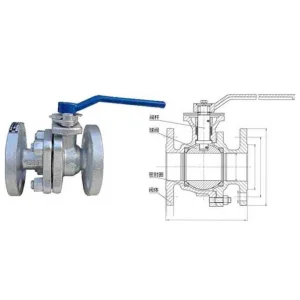
Wholesale American Standard Cast Steel Ball Valve Q41F-150LB
API/ASME standard flanged cast steel ball valves providing tight shut-off isolation for oil, water, and steam lines.
View Product Details →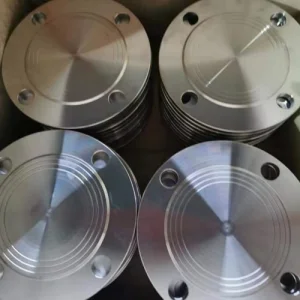
Discount SORF & WNRF Blind Flange Manufacturer & Factory Quotes
Slip-on raised face and weld neck raised face blind flanges engineered for high-temperature pressure vessel connections.
View Product Details →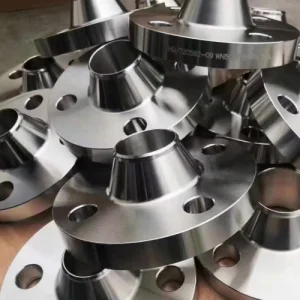
Best Flange Class 600 ASME B16.5 Suppliers & Export Company
Class 600 heavy pressure ASME B16.5 forged steel flanges featuring ring-type joint (RTJ) or raised face seating surfaces.
View Product Details →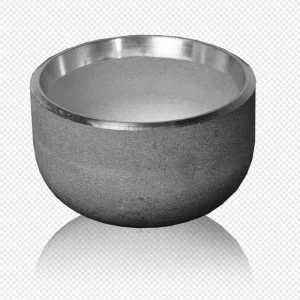
High-Quality 1 1/2" DN40 Carbon Steel Butt Weld High Pressure Cap
Precision seamless high-pressure pipe caps engineered to withstand extreme hydraulic impulse loads in process lines.
View Product Details →Frequently Asked Questions by Industrial Sourcing Specialists
Detailed technical insights regarding standards compliance, working pressure ratings, thread compatibility, and ordering procedures.
What is the main difference between Malleable Iron and Ductile Iron pipe fittings?
Malleable iron starts as white cast iron and achieves ductility via a multi-day post-casting thermal annealing process that converts iron carbide into irregular temper carbon clusters. Ductile iron achieves nodular graphite directly during casting through magnesium inoculation. Malleable iron excels in smaller threaded fittings (≤4 inches) due to its superior machinability, smooth casting finish, and precise thread execution, whereas ductile iron is predominantly used for larger flanged or push-on municipal water pipes.
Which standards govern malleable iron pipe fittings globally?
The dominant international standards include: ASME B16.3 (Malleable Iron Threaded Fittings Classes 150 & 300), ASME B16.39 (Malleable Iron Pipe Unions), EN 10242 / ISO 49 (Threaded Malleable Cast Iron Fittings), BS EN 1562 (Foundry Material Designations), and JIS B2301 (Japanese industrial threaded iron fittings).
What working pressure ratings apply to Class 150 and Class 300 malleable fittings?
Class 150 malleable iron fittings are rated for up to 300 psi (20.7 bar) for cold water/oil service (-29°C to 65°C) and 150 psi (10.3 bar) for saturated steam up to 186°C. Class 300 heavy-duty fittings are rated for up to 2000 psi (137.9 bar) for non-shock hydraulic service and 300 psi for saturated steam lines.
Can NPT threaded fittings mate directly with BSPT threads?
No, NPT and BSPT threads should not be interchanged without an adapter. NPT features a 60° thread flank angle with flat roots and crests, while BSPT (ISO 7-1) features a 55° thread angle with rounded roots and crests. Mating them directly will cause thread galling and leak paths under pressure.
What hot-dip galvanizing process is used for anti-corrosion protection?
Our factories utilize high-purity molten zinc baths maintained at 440°C–460°C. Castings undergo pickling and fluxing before immersion. The resulting zinc coating exceeds 70 microns (500 g/m²), creating a multi-layer metallurgical alloy bond (Gamma, Delta, Zeta, and Eta layers) that provides cathodic protection against severe atmospheric and underground corrosion.
How do I request Mill Test Certificates (MTC) and quality documentation?
All shipments are accompanied by EN 10204 Type 3.1 Inspection Certificates detailing exact chemical heats (C, Si, Mn, P, S), mechanical tensile and elongation test results, and 100% pneumatic hydro-test verification. You can request pre-shipment documentation directly through your dedicated export account engineer.
Global Sourcing Directory & Group Manufacturing Plants
Connect directly with our engineering sales leads in Cangzhou to request custom quotes, CAD drawings, and container pricing.
HEBEI CANGRUN PIPELINE EQUIPMENT CO., LTD
Group Headquarters & Export Center
- Bobei Industrial Zone, Cangzhou City, Hebei Province, China
- [email protected]
- +86 186 3384 2061 / +86 311 8701 7717
CANGZHOU FEIWO METAL PRODUCTS CO., LTD
Foundry Plant 1
- Boerzhuang Industrial Zone, Cangzhou City, Hebei Province, China
- [email protected]
- +86 139 3171 6210
CANGZHOU FEIXIANG METAL PRODUCTS CO., LTD
CNC & Tapping Division
- Boerzhuang Industrial Zone, Cangzhou City, Hebei Province, China
- [email protected]
- +86 130 1202 1525